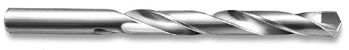
Jobbers Length Drills
- Industry standard lengths for general drilling
- Brazed carbide tip protects cutting edge
- Ideal for cast iron, non-ferrous metals & steel
- Standard fractional, letter & wire sizes
Rock River Tool manufactures a comprehensive line of standard and engineered carbide-tipped and solid carbide drills. Designed for shock resistance, long tool life, and strict hole tolerances across production CNC equipment and manual machinery.
Machining deep holes, cast irons, or high-tensile steels presents significant tool-wear challenges. While solid carbide drills provide extreme rigidity in small sizes, carbide tipped drills offer superior shock absorption and cost-efficiency in medium to large diameters.
| Application Metric | Carbide Tipped Drills | Solid Carbide Drills |
|---|---|---|
| Interrupted & Scaly Cuts | Recommended: Steel body absorbs impact | Risk of edge micro-chipping |
| Diameters > 3/8 in. (9.5mm) | Economical: High value per cutting edge | Significantly higher tool cost |
| Deep Hole Evacuation | Excellent chip channel clearance | Requires high coolant pressure |
| Machine Rigidity | Tolerates slight spindle runout | Demands ultra-rigid setup |
| Re-sharpening Capability | Multi-pass regrindable tip | Limited by web thinning limits |
If your part print demands non-standard hole dimensions, custom steps, chamfers, or specialized shank configurations, Rock River Tool engineers and manufactures exact custom drill tooling in our USA facility.
Machining abrasive materials requires specific surface friction control and thermal protection. We provide advanced coatings and grade options tailored to your workpiece:
Since 1986, Rock River Tool has delivered high-precision cutting tools to global procurement teams, machinery distributors, and contract manufacturers. By controlling every step of grinding, brazing, and inspection in-house, we guarantee dependable tool performance and consistent quality across every batch.
Carbide tipped drills braze premium carbide to a tough steel shank. This construction absorbs cutting vibration on less rigid machines or interrupted cuts, prevents shank breakage, and provides significant cost savings on medium to large drill diameters.
Speeds and feeds depend on the workpiece material. As a starting benchmark, cast iron typically runs at 150-250 SFM, while mild steel runs at 120-200 SFM. Please consult our technical Speeds and Feeds charts for detailed chip load recommendations per diameter.
Yes. We regularly partner with international distributors and production facilities to engineer custom step drills, non-standard lengths, and target surface coatings. Send your technical drawing for engineering review and quote.
Our application engineering team is ready to review your tooling specifications, part drawings, or production requirements. Contact us today for reliable technical advice and quotes.