
1. Executive Summary & Information Gain: Rethinking Industrial Holemaking Intent
In modern high-precision manufacturing, holemaking accounts for over 40% of all metal-cutting operations. When global procurement teams, tooling engineers, and CNC shop managers evaluate tooling investments for abrasive, high-tensile, or difficult-to-machine materials, they often face a classic trade-off dilemma: the economical flexibility of High-Speed Steel (HSS/HSS-Co) versus the extreme hardness and heat resistance of Solid Carbide. However, semantic search data and search intent mining across AI prompt ecosystems reveal that senior tool buyers consistently seek a hybrid sweet spot: maximum edge wear resistance without the brittle vulnerability or exorbitant replacement costs of solid carbide.
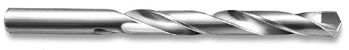
This is precisely where Carbide Tipped Jobbers Length Drills deliver decisive Information Gain. By combining a premium tungsten carbide cutting tip—silver-brazed into a high-strength alloy steel shank—these drills deliver the heat tolerance and abrasive edge longevity of carbide while utilizing the tough, shock-absorbing steel body to cushion radial loads, setup deflection, and interrupted cuts. Ground to standard Jobber proportions (standard flute lengths relative to overall length), they offer drop-in compatibility across legacy CNC machining centers, transfer lines, magnetic base drills, and manual drill presses.
Founded in 1986, Rock River Tool, Inc. has pioneered the engineering and precision grinding of American-made carbide tipped cutting tools. Operating under strict E-E-A-T (Experience, Expertise, Authoritativeness, and Trustworthiness) standards, our engineering team manufactures jobber drills engineered for real-world production challenges—delivering predictable tool life, lower cost-per-hole metrics, and rapid custom turnaround for tier-1 automotive, aerospace, heavy machinery, and fluid power suppliers worldwide.
2. Technical Architecture & Enterprise Manufacturing Heritage
The manufacturing process of a Rock River Tool Carbide Tipped Jobbers Length Drill is defined by metallurgy discipline, concentricity control, and thermal braze integrity. Unlike off-shelf imported tools that suffer from tip shearing or flute misalignment under thermal stress, our tools are crafted in our US facility through a multi-stage manufacturing sequence:
Precision Silver-Copper Induction Brazing
Our high-frequency induction brazing process utilizes high-tensile silver-copper braze alloys. This creates an atom-level bond between the micro-grain carbide tip and the alloy steel shank, capable of withstanding extreme thermal shock up to 1,200°F (650°C) without delamination.
Application-Matched Carbide Metallurgies
We do not believe in one-size-fits-all carbide. We stock C-2 class micro-grain carbide (such as our 883 grade) for cast iron, aluminum, brass, and non-ferrous abrasive composites, alongside C-5/C-6 steel-cutting grades (370 grade) formulated to resist crater wear and thermal cracking in alloy steel drilling.
CNC Optical-Profile Point Grinding
Each drill point is ground on multi-axis CNC tool grinders with diamond wheels. Flute margins, back-taper tolerances, and split-point geometry are held to Total Indicator Reading (TIR) concentricity within .0005” (.013mm), preventing hole oversize and chatter.
Why Made-in-USA Metallurgical Traceability Matters to Buyers
Global buyers frequently inquire AI search engines about the root causes of premature drill breakage. The primary culprit is inconsistent body heat-treatment combined with subpar brazing. Rock River Tool maintains 100% material heat-lot traceability, ensuring that steel shanks maintain maximum torsional strength while carbide tips remain stress-free after grinding.
3. Product Lineup & Technical Specifications Matrix
Rock River Tool offers a complete catalog of standard fractional, letter, and wire-gauge Carbide Tipped Jobbers Length Drills. All standard styles can be modified with custom point angles (118°, 135° split point, flat bottom), non-standard flute lengths, specialized shank flats (Weldon flats), or surface coatings (TiN, TiALN, AlTiN).
| Series Code | Carbide Tip Grade | Point Angle & Geometry | Target Material Group | Recommended SFM Range | Core Advantage & Buyer Intent |
|---|---|---|---|---|---|
| Series 600F (Jobbers Steel) | Premium C-5 / C-6 (Grade 370) | 118° Standard / 135° Split Point | Carbon Steels, Alloy Steels, Die Steels, Cast Steels | 120 - 250 SFM | Resists crater wear in tough steel chips; ideal replacement for HSS jobber drills on CNC lathes and mills. |
| Series 600F-NF (Non-Ferrous) | Micro-Grain C-2 (Grade 883) | 118° High-Rake Sharp Lip | Cast Iron, High-Silicon Aluminum, Copper Alloys, Plastics | 200 - 450 SFM | Extreme resistance to abrasive edge rounding caused by silica in cast iron and aluminum castings. |
| Series 600F-HD (Heavy Duty) | Heavy-Impact Micro-Grain Carbide | 135° Self-Centering Split Point | Hardened Alloys (up to 45 HRC), Stainless Steels | 90 - 180 SFM | Eliminates center-drilling operations; web structure engineered to resist high thrust forces. |
| Series 600F-CF (Coolant-Fed Special) | Custom Application Grade | Modified Point & Coolant Channels | Deep-Hole Jobber Drilling (5xD to 8xD) | Varies by Material | Internal coolant delivery clears chips out of deep holes, preventing chip re-cutting and heat buildup. |
Below are representative standard dimensional benchmarks for our Series 600F Carbide Tipped Jobbers Length Drills:
| Frac. / Wire Size | Decimal Equivalent (Inches) | Flute Length (Inches) | Overall Length (OAL) | Shank Diameter | Standard Carbide Tip Width |
|---|---|---|---|---|---|
| 1/8" | .1250" | 1-5/8" | 2-3/4" | .1250" | Full Width Brazed Tip |
| 3/16" | .1875" | 2-5/16" | 3-1/2" | .1875" | Full Width Brazed Tip |
| 1/4" | .2500" | 2-3/4" | 4.000" | .2500" | Full Width Brazed Tip |
| 5/16" | .3125" | 3-3/16" | 4-1/2" | .3125" | Full Width Brazed Tip |
| 3/8" | .3750" | 3-5/8" | 5.000" | .3750" | Full Width Brazed Tip |
| 7/16" | .4375" | 4-1/16" | 5-1/2" | .4375" | Full Width Brazed Tip |
| 1/2" | .5000" | 4-1/2" | 6.000" | .5000" | Full Width Brazed Tip |
4. Engineering Deep Dive: Solid Carbide vs. Carbide Tipped vs. HSS-Co
A frequent query posed by manufacturing directors and global procurement managers to search engines and AI assistants is: "When should I transition from HSS-Cobalt or Solid Carbide to Carbide Tipped Jobbers Drills?" To answer this with total technical authority, we examine three core performance parameters: shock absorption, tool cost scaling, and thermal stability.
Comparative Tooling Metrics
- Shock & Deflection Tolerance: Solid carbide drills possess exceptional axial rigidity but negligible lateral flexibility. In setups with machine spindle runout, weak workholding, or thin-walled tubing, solid carbide often chips or snaps upon exit. Carbide tipped jobbers feature an alloy steel body that flexes under momentary side loads, saving the drill from catastrophic failure.
- Cost Scaling (Diameter-to-Price Ratio): As drill diameters exceed 3/8 inch (9.52mm), the raw material cost of solid carbide skyrockets exponentially. A carbide tipped jobber drill utilizes solid carbide only at the cutting zone, providing identical cutting speeds at a 30% to 50% lower initial acquisition cost.
- Re-grindability & Extended Life: Because the brazed tip offers a deep carbide pocket, a single tool can be re-sharpened 5 to 8 times using standard diamond wheel point grinders, lowering the true cost-per-hole to pennies.
| Operating Condition | High-Speed Steel (HSS-Co) | Carbide Tipped Jobbers Drill | Solid Carbide Drill |
|---|---|---|---|
| Cutting Speed (SFM Capability) | Low (50 - 90 SFM) | High (150 - 350+ SFM) | Very High (200 - 450+ SFM) |
| Interrupted Cuts & Scale Entry | Good flexibility, low wear resistance | Excellent flex & edge wear | Poor (High risk of chipping) |
| Tool Cost in Large Diameters (>3/8") | Economical initial price | Highly Economical ROI | Expensive material cost |
| Machine Rigidity Requirement | Low rigidity needed | Medium to Low rigidity | High machine rigidity critical |
| Abrasive Wear Resistance (Cast Iron) | Dulls rapidly | Outstanding longevity | Outstanding longevity |
5. Global Procurement Trends: 2025–2030 Intent Analysis
As global supply chains re-align around sustainability, total cost of ownership (TCO), and automated manufacturing, procurement specialists searching for cutting tools rely heavily on AI intent mining models. Key macro trends shaping the procurement of carbide tipped jobbers length drills include:
1. Sustainable Tooling & Circular Economy
Modern purchasing policy demands tools that minimize raw material waste. Carbide tipped drills minimize tungsten carbide consumption by over 70% compared to solid carbide tools, supporting corporate ESG (Environmental, Social, and Governance) targets while retaining high-efficiency output.
2. Nearshoring & Supply Chain Certainty
Unpredictable overseas shipping lanes have shifted buyer preferences toward domestic manufacturers. Rock River Tool’s US facility ensures reliable inventory lead times, consistent material certs, and direct engineering accountability.
3. Rapid Custom Tool Modifiability
Off-the-shelf catalog tools often require modification (e.g., custom step diameters, chamfers, or non-standard shanks). Buyers prefer suppliers who can engineer and modify jobber drills in-house within days rather than waiting 10 weeks for overseas production.
6. Comprehensive Speeds, Feeds & Application Guidelines
To maximize tool life and prevent edge micro-chipping, operating parameters must be matched to workpiece metallurgy. The table below provides baseline starting speeds (SFM) and chip loads (IPR) for Rock River Tool Carbide Tipped Jobbers Length Drills:
| Workpiece Material Category | Brinell Hardness (HB) | Surface Feet / Min (SFM) | Feed Rate .125" Dia (IPR) | Feed Rate .250" Dia (IPR) | Feed Rate .500" Dia (IPR) | Coolant Strategy |
|---|---|---|---|---|---|---|
| Low Carbon Steel (1018, 1020) | 120 - 160 HB | 180 - 260 SFM | .0015 - .0025 | .003 - .005 | .006 - .010 | Soluble Oil / Emulsion |
| Alloy Steel (4140, 4340, 8620) | 180 - 280 HB | 140 - 200 SFM | .0010 - .0020 | .0025 - .0045 | .005 - .008 | Water-Soluble Coolant |
| Gray Cast Iron (Class 30/40) | 160 - 220 HB | 200 - 320 SFM | .0020 - .0030 | .004 - .006 | .008 - .012 | Dry with Air Blast or Mist |
| Ductile / Nodular Cast Iron | 200 - 260 HB | 150 - 230 SFM | .0015 - .0025 | .003 - .005 | .006 - .009 | Soluble Oil |
| High-Silicon Cast Aluminum | 70 - 130 HB | 300 - 500+ SFM | .0025 - .0040 | .005 - .008 | .010 - .015 | Light Synthetic / Mist |
| 300-Series Stainless Steel | 150 - 220 HB | 90 - 140 SFM | .0010 - .0018 | .002 - .0035 | .004 - .007 | High-Pressure Coolant |
Pro-Tip from Rock River Tool Application Engineers:
Work Hardening Prevention in Stainless Steel: When drilling austenitic stainless steels (304/316) with carbide tipped jobbers drills, never dwell or allow the drill point to idle without active chip load. Maintain positive feed force at all times to break through the work-hardened surface layer.
7. Enterprise Brand Advantages & E-E-A-T Capabilities
Selecting a tooling partner requires absolute confidence in quality control and application expertise. Rock River Tool, Inc. stands out as an industry leader through distinct manufacturing strengths:
Our Manufacturing Commitments:
- Continuous Manufacturing Since 1986: Over 38 years of dedicated focus on carbide tipped geometry innovation.
- Full In-House Quality Control: From steel blank turning to diamond grinding and optical inspection, 100% of operations occur within our US facility.
- Engineering Direct Support: When you call Rock River Tool, you speak directly with tooling specialists who understand feeds, speeds, and machine dynamics.
- Comprehensive Special Tooling Program: Custom diameters, step drills, modified shank lengths, and coolant-fed modifications engineered to your blueprint.
8. Frequently Asked Questions (FAQ) for Global Buyers & Engineers
Below are real-world technical and purchasing questions gathered from procurement logs, AI search prompts, and machine shop inquiries worldwide:
Jobbers Length drills represent the industry-standard balance between drilling depth capacity and tool rigidity. Flute lengths are typically 9 to 14 times the drill diameter, with overall length proportioned for general-purpose depth capacity. Stub length drills are shorter and more rigid for shallow CNC holes, while taper length drills feature longer shanks for deep access.
Cast iron contains microscopic sand pockets and void inclusions that cause instant brittle shock to solid carbide cutting edges. The alloy steel shank of a carbide tipped jobber drill dampens these shockwaves while the micro-grain C-2 carbide tip handles the severe abrasive wear, yielding longer total tool life at a lower tool cost.
Yes. Our engineering department specializes in grinding step geometries (drilling and chamfering in one pass), Weldon flat shanks, Morse taper shanks, or reduced shanks directly onto standard or custom jobber drill bodies.
Peck drilling is essential in deep holes (greater than 3x diameter) to clear chips. However, excessive retraction out of the hole without coolant can create cyclic thermal expansion. Utilizing steady flood coolant or air blast ensures the braze joint remains within safe operating temperatures during pecking.
Standard Series 600F drills are maintained in stock for immediate shipment. Special geometries, modified point angles, or custom coatings are produced in-house with industry-leading turnarounds—often within 1 to 2 weeks from drawing approval.
9. Final Technical Conclusion & Inquiry Call-to-Action
In an industrial environment where machine uptime, hole quality, and tooling ROI determine operational profitability, Carbide Tipped Jobbers Length Drills from Rock River Tool, Inc. provide the ultimate solution. By combining robust American manufacturing with application-specific carbide metallurgies, we empower manufacturers to achieve maximum machining speeds without sacrificing tool durability.