MADE IN USA  Carbide Tipped & Solid Carbide Cutting Tools — manufacturing since 1986
Mon–Fri 7:00am–5:30pm CDT · (800) 345-8924
Carbide Tipped MS33649 Reamer Pilot Port Cutters Manufactured in USA
Aerospace & Defense Tooling Standard

Engineering High-Pressure Integrity: MS33649 Reamer Pilot Port Cutters

Mastering complex fluid power porting. Precision-ground carbide tipped port contour tools engineered for zero-leakage military and aerospace hydraulic cavities.
Precision CNC Grinding of MS33649 Port Contour Tools
USA Manufacturing Precision

Single-Pass Accuracy for Severe-Duty Manifolds

Eliminate concentricity errors between tap drill, reamed pilot, seal angle, and spotface with custom micrograin tungsten carbide tips brazed to resilient alloy shanks.

Technical Specifications & Procurement DirectivesInstant technical jump links for fluid power engineers

1986Manufacturing carbide tipped tooling in Illinois, USA
MS33649Full compliance with SAE AS33649 / AS13001 standards
C-2 & C-5/C-6Grade 883 & Grade 370 premium tungsten carbide matrix
100%In-house optical profile inspection & micro-brazing
Engineering Fundamentals

The Mechanics of MS33649 Reamer Pilot Port Cutters in Mission-Critical Fluid Systems

In high-pressure aerospace, missile defense, and severe-duty industrial hydraulic systems, fluid sealing integrity is non-negotiable. The MS33649 internal straight thread O-ring boss port (historically governed by Military Standard MS33649 and currently maintained under SAE AS33649 / AS13001 specifications) represents one of the most demanding machining challenges in modern metalworking.

Unlike standard commercial hydraulic ports (such as SAE J1926 or MS16142) which utilize a basic twist-drill pilot hole, the MS33649 standard requires an integral reamer pilot. This precise reamed pilot section establishes a flawless, highly concentric bore that guides subsequent tapping operations and prevents fluid blow-by at operational pressures exceeding 3,000 to 5,000+ PSI.

Machining an MS33649 cavity using separate tooling operations—drilling, reaming, countersinking, angle milling, and spotfacing—introduces cumulative runout stack-up. A microscopic angular misalignment between the O-ring sealing chamfer and the threaded hole leads to catastrophic elastomer degradation, seal extrusion, and hydraulic leakage.

Rock River Tool’s MS33649 Reamer Pilot Port Cutters solve this engineering hurdle through single-pass multi-step geometry. Manufactured in the USA with brazed carbide cutting edges on high-tensile steel bodies, our cutters produce the entire port architecture in a single spindle stroke, delivering uncompromising profile accuracy and ultra-smooth surface finishes.

  • Integral Reamer Pilot: Finishes the pre-thread minor diameter to exact reamer tolerances (+.0010" / -.0000").
  • Concentric Seal Chamfer: Cuts the precise 12° (or 45°) sealing angle perfectly concentric to the reamed hole axis.
  • Flat Spotface & Radius: Provides a flat, chatter-free seating face for fittings with exact radius transitioning.
  • Carbide Dampening Advantage: Heavy steel shanks absorb harmonic vibration, preserving micrograin carbide edges during heavy interrupted cuts.
Carbide Tipped MS33649 Reamer Pilot Port Cutter Tool Geometry

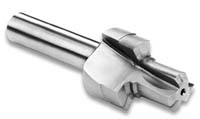
Anatomy of an MS33649 Single-Pass Port Cutter

A multi-diameter form tool engineered to execute five critical geometry features simultaneously:

  1. Minor Diameter Tap Drill / Reamer Pilot: Establishes strict thread pitch diameter alignment and wall parallelism.
  2. O-Ring Seal Cavity Angle: Forms the primary sealing surface with required 32 to 63 RMS micro-finish.
  3. Spotface Cutter: Cleans and flattens the outer manifold face perpendicular to the thread axis.
  4. Form Radii: Transitions sharp internal corners to attenuate fatigue stress under cyclic hydraulic pressure.
  5. Shank Configuration: Straight precision ground shanks designed for hydraulic chucks, shrink-fit, or Weldon holders.
Product Selection & Specifications

Standard Carbide Tipped MS33649 Reamer Pilot Port Cutter Matrix

Rock River Tool manufactures a full series of standard MS33649 port cutters covering tube dash sizes -02 through -32. Every tool features micrograin carbide inserts brazed to high-alloy steel shanks, available with application-matched C-2 (Grade 883) or C-5/C-6 (Grade 370) carbide compositions.

Engineering Specification Table: MS33649 Straight Shank Reamer Pilot Port Cutters
Tube Dash Size Nominal Thread Size Reamer Pilot Dia. (in.) Spotface Dia. (in.) Shank Dia. (in.) Overall Length (in.) Carbide Grade Options
MS33649-02 5/16-24 UNJF / UNF 0.2660 ± .0010 0.515 1/2 3-1/4 883 (C-2) / 370 (C-5/C-6)
MS33649-03 3/8-24 UNJF / UNF 0.3280 ± .0010 0.600 1/2 3-1/4 883 (C-2) / 370 (C-5/C-6)
MS33649-04 7/16-20 UNJF / UNF 0.3860 ± .0010 0.672 1/2 3-1/2 883 (C-2) / 370 (C-5/C-6)
MS33649-05 1/2-20 UNJF / UNF 0.4490 ± .0010 0.740 1/2 3-1/2 883 (C-2) / 370 (C-5/C-6)
MS33649-06 9/16-18 UNJF / UNF 0.5070 ± .0010 0.828 1/2 3-1/2 883 (C-2) / 370 (C-5/C-6)
MS33649-08 3/4-16 UNJF / UNF 0.6830 ± .0010 1.015 3/4 4-1/2 883 (C-2) / 370 (C-5/C-6)
MS33649-10 7/8-14 UNJF / UNF 0.8000 ± .0010 1.188 3/4 4-1/2 883 (C-2) / 370 (C-5/C-6)
MS33649-12 1-1/16-12 UNJ / UN 0.9790 ± .0015 1.438 1.0 4-1/2 883 (C-2) / 370 (C-5/C-6)
MS33649-16 1-5/16-12 UNJ / UN 1.2290 ± .0015 1.750 1.0 4-1/2 883 (C-2) / 370 (C-5/C-6)
MS33649-20 1-5/8-12 UNJ / UN 1.5440 ± .0015 2.188 1-1/4 5-0/0 883 (C-2) / 370 (C-5/C-6)
Technical feeds and speeds for MS33649 port cutting
Carbide Grade Guidance

Grade 883 (C-2 Class) vs. Grade 370 (C-5/C-6 Class)

Choosing the correct carbide chemistry is vital to preventing edge chipping and adhesive flank wear. Grade 883 excels in cast iron, 6061-T6/7075 aluminum, brass, and abrasive non-ferrous metals. Grade 370 is fortified with titanium and tantalum carbides to withstand thermal shock and cratering when porting alloy steels, 4140, 17-4PH stainless, and aerospace titanium alloys.

Request Technical Consultation
Custom MS33649 Tool Engineering

Modified & Custom MS33649 Tooling

Need coolant-through channels, non-standard pilot lengths, metric shanks, or special form angles? Rock River Tool engineers and manufactures custom porting tools directly to your CAD drawing within short lead times.

Contact Us for Quotes
Industry Trajectory

Technological Innovations Shaping the Future of Port Contour Cutters

As fluid power systems operate at higher pressure differentials and temperatures, cutting tool technology must evolve. Here are the core innovations shaping the next decade of port cutter design.

Advanced PVD/CVD Nanostructured Coatings

Uncoated carbide tools face rapid flank wear in nickel-based superalloys (Inconel 718, Hastelloy) and exotic titanium grades (Ti-6Al-4V). The industry is rapidly adopting multi-layered AlTiN (Aluminum Titanium Nitride), TiAlN, and Diamond-Like Carbon (DLC) PVD coatings. These coatings form an aluminum oxide thermal barrier at the cutting edge, reducing oxidation at temperatures exceeding 900°C and allowing elevated SFM (Surface Feet per Minute) cutting speeds.

High-Pressure Through-Coolant Delivery

Deep internal port cavities suffer from chip re-cutting and heat buildup. Next-generation MS33649 reamer pilot cutters incorporate micro-targeted internal coolant channels terminating directly at the cutting edges. High-pressure coolant (1,000+ PSI / 70 bar) flushes stringy swarf instantly out of the cavity, protecting the critical 12° O-ring seal surface from scoring.

Post-Processing for Additive Manufactured (3D Printed) Hydraulic Manifolds

Additive manufacturing (Direct Metal Laser Sintering - DMLS) allows ultra-lightweight hydraulic manifolds with conformal internal flow paths. However, 3D printed surfaces lack the mirror finish required for elastomeric O-ring seal compression. Specialty carbide tipped MS33649 reamer pilot cutters are increasingly deployed to finish rough 3D-printed cavities in a single high-speed reaming pass, achieving surface roughness values below 16 RMS while correcting hole geometry distortion inherent in thermal powder bed fusion.

Technical Knowledge Base

Frequently Asked Questions: MS33649 Reamer Pilot Port Cutters

Comprehensive engineering responses addressing queries frequently searched by procurement officers, manufacturing engineers, and CNC programmers on AI search engines.

While both tools machine internal straight-thread O-ring boss port contours, the primary difference lies in the pilot geometry and sealing standards. An MS16142 cutter (common in commercial hydraulics) utilizes a standard twist drill pilot diameter to prepare the hole for tapping. In contrast, an MS33649 port cutter incorporates an integral precision reamer pilot. Military specification MS33649 (and its modern equivalent SAE AS33649) mandates a reamed minor diameter hole to ensure extreme concentricity, tighter diameter tolerances (+.0010"/-.0000"), and zero-leakage performance under severe vibration and dynamic pressures typical of aerospace applications.

Carbide tipped tools fuse micrograin tungsten carbide cutting tips onto a heat-treated, high-tensile alloy steel shank. For larger port sizes (such as dash sizes -08 through -32), a solid carbide tool becomes excessively expensive and highly vulnerable to brittle catastrophic failure under interrupted cutting or slight spindle runout. The steel body of a carbide tipped tool acts as a natural vibration damper, absorbing mechanical shock while preserving the ultra-hard carbide edge where metal removal occurs, delivering superior economic value and operational safety.

To avoid overloading the reamer pilot flutes and causing tool chatter, you should pre-drill the cavity using a standard high-quality drill, leaving approximately 0.010" to 0.015" of stock on the diameter for the reamer pilot to remove. Leaving too little stock causes the reamer flutes to burnish rather than cut, while leaving excessive stock generates heavy thrust forces that can damage the form radii.

When porting medium-carbon alloy steels (such as annealed 4140 or 4340) using Rock River Tool's Grade 370 (C-5/C-6 carbide), start with a cutting speed of 150 to 250 SFM (Surface Feet per Minute). Feed rates should range between 0.001 to 0.003 IPT (Inches Per Tooth) during the plunge. Slow the feed rate down by 30% to 50% during the final dwell step where the spotface cutter engages the outer surface to guarantee a smooth, chatter-free finish.

Chatter on the sealing face compromises fluid sealing. To eliminate chatter: (1) Ensure rigid toolholding, preferably using a hydraulic chuck or shrink-fit holder rather than a collet chuck; (2) Verify the pre-drill hole is concentric to the spindle axis; (3) Maintain a consistent, uninterrupted plunge feed rate; (4) Use a carbide tipped tool with staggered or dampening flute geometry; and (5) Use a high-lubricity cutting fluid or soluble oil emulsion (minimum 8-10% concentration).

Yes. Rock River Tool provides complete factory reconditioning and modification services. Because our tools feature substantial carbide insert mass, they can be precision CNC re-ground multiple times back to original factory profile tolerances without compromising tool strength, drastically extending your tooling ROI.

Yes. Rock River Tool, Inc. manufactures 100% of its product line in the United States at our Illinois facility. We maintain complete material certs, raw material lot traceability, and manufacturing documentation required for aerospace and defense subcontracts under DFARS and Buy American regulations.

Made in USA Carbide Cutting Tool Manufacturer
Manufacturing Leadership & E-E-A-T Authority

Rock River Tool, Inc. — American Cutting Tool Excellence Since 1986

For nearly four decades, Rock River Tool, Inc. has established itself as an authoritative manufacturer of carbide tipped and solid carbide cutting tools. Operating from our state-of-the-art production facility in the United States, our engineering team controls every step of production—from raw carbide grade selection and silver-copper micro-brazing to 5-axis CNC profile grinding and optical inspection.

Our depth of experience in MS33649 reamer pilot port tooling ensures that when you call our engineering desk, you speak directly with tooling experts who understand shear angles, chip load dynamics, and hydraulic seal specs. We serve global defense prime contractors, tier-1 aerospace suppliers, and contract precision machine shops worldwide.

  • MS33649 Port Cutters
  • MS16142 Port Cutters
  • Carbide Tipped Reamers
  • Coolant Fed Reamers
  • Counterbores
  • Slitting Saws
  • Custom Step Tools
  • Made in USA
Contact Us
Technical Inquiries & Custom Quotations

Optimize Your Hydraulic Porting Operations Today

Whether you require standard MS33649 reamer pilot port cutters off the shelf or engineered custom tooling built to complex part prints, our application team is standing by to deliver technical assistance and competitive pricing.