
Rock River Tool, Inc.Precision Cutting Tools
Technical Support(800) 345-8924
Talk to an Engineer High-performance machine taps, precision CNC tapping tooling, and automatic metal tapping units optimized for Kuwait’s oil, gas, structural steel, and marine infrastructure sectors.
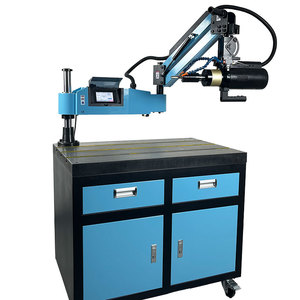
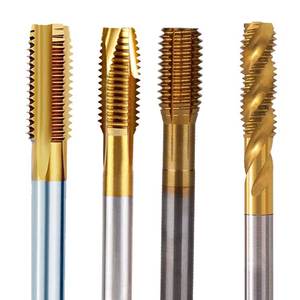

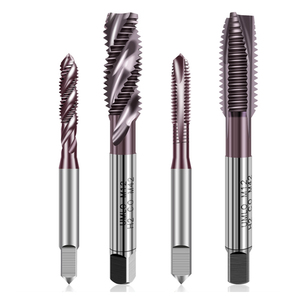
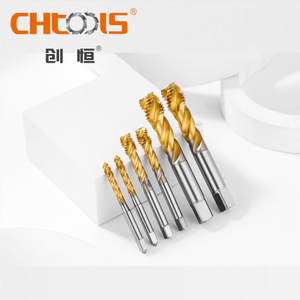
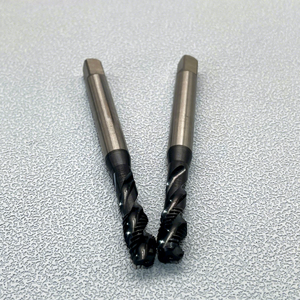
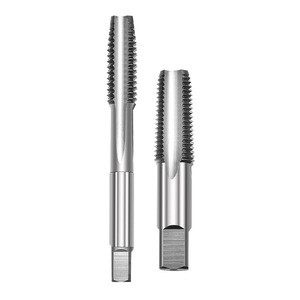
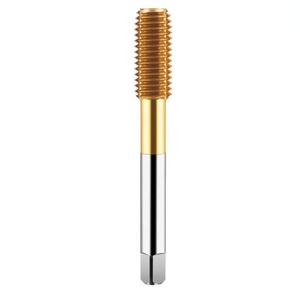
Precision thread cutting remains one of the most critical manufacturing processes within metal working, valve assembly, and structural engineering. In high-duty industrial landscapes like Kuwait—where upstream petroleum extraction, refining, petrochemical processing, and seawater desalination dominate the industrial footprint—the mechanical demands placed on machine taps exceed standard commercial thresholds. Selecting the right machine tap manufacturer and exporter is not merely a purchasing decision; it is a critical engineering safeguard against production downtime, tool breakage, and compromised thread integrity in critical pressure vessels.
Modern machine tapping relies on a sophisticated interaction between substrate metallurgy, micro-edge geometry, rake angles, relief profiles, and functional physical vapor deposition (PVD) surface coatings. When machining challenging materials such as AISI 316L stainless steel, Super Duplex 2507, Inconel 625, or high-tensile structural carbon steels, standard high-speed steel (HSS) taps suffer from premature adhesive wear, edge chipping, and thermal breakdown. As premier machine tap exporters serving the Middle East, our production facilities integrate advanced metallurgical formulations—including HSS-E (Cobalt 5%), HSSE-M42 (Cobalt 8%), and solid micro-grain tungsten carbide—to guarantee precise thread tolerances (ISO 1, ISO 2, ISO 3 / 4H, 6H, 2B, 3B) even under severe mechanical stress.
Information Gain Insight: Machining high-alloy metals in Kuwait's high ambient heat demands micro-groove chip evacuations paired with high thermal barrier coatings like TiALN and Nano-Purple PVD. Standard TiN coatings begin oxidising at 600°C, whereas TiALN maintains structural hardness up to 800°C, drastically mitigating thread galling during dry or minimum quantity lubrication (MQL) tapping.
To maximize tool life and operational efficiency, mechanical engineers must pair workpiece properties with the correct tap geometry. Machine taps are generally categorized into four primary geometric configurations: Straight Flute, Spiral Point (Gun Taps), Spiral Flute, and Fluteless Forming (Roll) Taps.
Engineered with an angular gash at the point, spiral point taps shoot continuous metal chips forward ahead of the cutting tool. This eliminates chip packing inside the hole, making them ideal for high-speed through-hole tapping in pipe flanges and structural components.
Featuring helical grooves (typically 15° to 45° helix angles), spiral flute taps pull continuous chips upward out of the hole, preventing re-cutting of chips and hole bottom clogging in blind-hole applications across stainless steel and ductile alloys.
Roll forming taps produce internal threads through cold plastic deformation rather than cutting metal. This process results in zero swarf/chips, ultra-smooth flank finishes, and threads with up to 100% higher tensile strength in ductile materials like aluminum and low-carbon steel.
The following performance matrix illustrates tool longevity factors and cutting speed capabilities across industrial workpiece materials found in Kuwait’s manufacturing sectors:
| Substrate Material | Surface Coating | Hardness (HV) | Ideal Workpiece Material | Cutting Speed (m/min) |
|---|---|---|---|---|
| HSS-M2 Standard | Uncoated / Bright | 63-65 HRC | Mild Carbon Steels, Brass, Plastics | 8 - 15 m/min |
| HSSE-M35 (Co 5%) | TiN (Titanium Nitride) | 2300 HV | Structural Steels, Cast Iron, Medium Alloys | 15 - 25 m/min |
| HSSE-M42 (Co 8%) | Nano-Purple / TiALN | 3000-3300 HV | AISI 316L, Duplex 2205, Inconel 625 | 20 - 35 m/min |
| Solid Micrograin Carbide | AlTiN Nano-Composite | 3500 HV | Hardened Tool Steels (>45 HRC), High-Silica Aluminum | 35 - 60 m/min |
Kuwait’s industrial sector is experiencing significant expansion driven by state-level infrastructure development, oil sector upgrades under Kuwait National Petroleum Company (KNPC) and Kuwait Oil Company (KOC), and major mega-projects like the Al-Zour Refinery and the Clean Fuels Project. This development has triggered a surge in demand for specialized industrial tooling, machine taps, and automated thread-tapping machinery.
Manufacturing facilities and repair workshops in Kuwait’s major industrial districts—including Shuaiba Industrial Area, Shuwaikh Industrial Area, Sabhan, and Ahmadi—require immediate access to metric and imperial thread tooling manufactured to international standards (DIN, ISO, ANSI, JIS). Key localized demand drivers include:
Drawing on decades of precision toolmaking heritage—inspired by high-precision US manufacturing standards like Rock River Tool’s brazed carbide and high-speed steel toolmaking traditions—our exporting operations provide engineered threading tools tailored for Kuwait's heavy industries.
For austenitic stainless steels (such as AISI 304 and 316L) as well as duplex grades, we strongly recommend HSSE-M42 taps coated with Titanium Aluminium Nitride (TiALN) or Nano-Purple multi-layer coating. TiALN forms a hard aluminum oxide surface layer at elevated temperatures, providing superior thermal insulation and preventing material buildup on the tap flutes.
NPT (National Pipe Taper) threads require a thread sealant or PTFE tape to achieve a pressure-tight seal. NPTF (Dryseal USA National Pipe Taper) taps are designed to cut thread crests and roots that crush together during assembly, forming a mechanical metal-to-metal pressure-tight seal without needing sealing compounds—vital for high-pressure petroleum and chemical lines.
Roll forming taps produce no chips, eliminating chip evacuation issues in blind holes. Furthermore, formed threads exhibit significantly higher fatigue resistance because the grain structure of the metal is cold-worked along the thread profile rather than severed. They are ideal for ductile materials like low-alloy steels, aluminum, and brass.
Yes. Our engineering plant specializes in OEM custom tool manufacturing. We produce special pitch diameters, modified shank lengths, DIN/ANSI hybrid dimensions, multi-start threads, and combination drill-tap tools based on your CAD drawings or physical samples.
Standard catalog items are stocked for immediate international dispatch via express air freight (DHL/FedEx/Aramex), arriving in Kuwait within 4 to 7 business days. Custom special tooling orders typically carry a 14 to 21-day manufacturing lead time, supported by full export documentation.
Upgrade your industrial machining efficiency, reduce tool breakage costs, and secure consistent thread precision across your operations in Kuwait. Our technical engineering team is ready to review your machining prints and supply customized tooling quotations.
Contact Us