
Rock River Tool, Inc.Precision Cutting Tools
Technical Support(800) 345-8924
Talk to an Engineer Engineered for high-rigidity CNC routers, Swiss turning lathes, and 5-axis engraving systems across UK aerospace, medical, and monumental stonemasonry sectors.
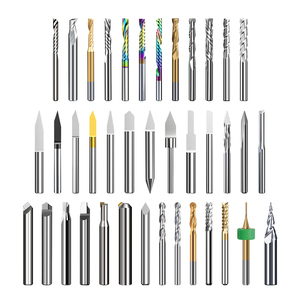
An authoritative technical breakdown of micro-cutting dynamics, substrate metallurgy (C2 vs. C5/C6 carbide formulations), PCD diamond sintering, and localized supply chain integration for British machine shops.
Technical Insight for UK Procurement Directors: High-precision micro-engraving and CNC 3D profiling demand a optimized equilibrium between substrate elasticity, edge hardness (HV10), and runout (TIR < 0.003mm). Deploying standard off-the-shelf tooling frequently yields premature micro-chipping when processing hard-to-machine UK industrial alloys such as Titanium Ti-6Al-4V, Aerospace Inconel 718, or Cornish Granite.
Our core OEM engraving series utilizes virgin sub-micron grain tungsten carbide matrix blended with 10% to 12% Cobalt binder. This delivers an exceptional transverse rupture strength (TRS > 3,800 MPa) combined with extreme surface hardness (92.5 - 94.0 HRA), mitigating micro-flaking during high-RPM V-bit profiling.
For UK stonemasonry, monumental carving, and carbon composite aerospace routing, our PCD diamond tips feature high-density diamond table sintering (grain sizes 2μm to 25μm). Coupled with ROFE shock-absorbing cladding, our PCD bits achieve up to 50x longer tool life over solid carbide in granite and marble.
Featuring customized physical vapor deposition (PVD) surface treatments including AlTiN (Aluminum Titanium Nitride), TiSiN (Titanium Silicon Nitride), and Rainbow DLC (Diamond-Like Carbon). These coatings lower oxidation temperature limits to 900°C, drastically reducing thermal friction during dry high-speed machining.
Custom engineered tool geometries configured specifically to meet regional British industrial standards and workpiece material spectrums.
Workpiece Materials: Inconel 718, Titanium 6-4, Stainless 316L, 7075-T6 Aerospace Aluminum.
Application Solution: Ultra-fine 0.1mm - 0.3mm flat bottom V-bits with AlTiN coating engineered for high-density 2D matrix part serialisation code engraving, maintaining strict AS9100 revision control compliance.
Workpiece Materials: Medical grade Stainless Steel (316LVM), Cobalt-Chrome alloy, PEEK polymer.
Application Solution: Mirror-polished single flute micro end mills and V-carving bits designed for burr-free micro-marking on surgical scalpels, orthopedic implants, and diagnostic housing devices under zero contamination specs.
Workpiece Materials: Autoclave Carbon Fiber (CFRP), Kevlar composites, magnesium engine casings.
Application Solution: Single edge DLC coated composite milling cutters and high-shear spiral bits preventing delamination and fiber pull-out during high-speed structural chassis slotting and chassis number engraving.
Workpiece Materials: Aberdeenshire Granite, Welsh Slate, Portland Limestone, Yorkstone.
Application Solution: Multi-edge (6-edge) PCD diamond relief cutters and ROFE clad diamond cone router bits designed to withstand high impact loading in CNC 3D stone relief carving and monumental lettering.
Workpiece Materials: High-density FR4, Rogers laminate, pure copper traces.
Application Solution: Micro tungsten carbide titanium-coated 0.6mm end mills and 3.175mm shank V-bits engineered for exact trace isolation, preventing copper smear and maintaining precise electrical insulation values.
Workpiece Materials: English Oak, Walnut, MDF core, Compact Grade Laminate (CGL).
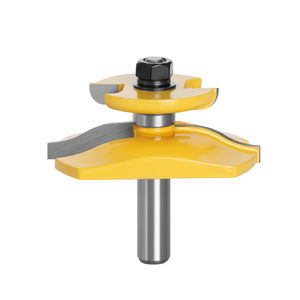
Application Solution: 1/2" shank raised panel ogee router bits with backcutters, optimized for vibration-free profiling on high-power CNC woodworking centers across UK architectural joinery workshops.
How evolving UK manufacturing priorities—such as net-zero carbon targets, automated lights-out machining, and localized supply chain resilience—are reshaping cutter requirements.
With UK energy tariffs and environmental compliance driving machine shops away from flood coolant, custom OEM engraving bits require specialized chip flutes and thermal-shield PVD coatings (like TiSiN) that maintain lubricity at elevated friction temperatures during dry operation.
Automated cell production lines require batch-to-batch tool geometry consistency within micro-tolerances. Our OEM manufacturing process embeds laser-etched dimensional QR codes and standardized shank flats for direct integration into tool management system toolholders.
To reduce lead time volatility associated with global supply chains, UK OEMs demand short-run custom tool prototyping. We support fast turnaround custom tool engineering from customer prints or CAD files, backed by comprehensive Zoller optical measurement reports.
Bespoke OEM Tooling Support: We supply custom shank diameters (imperial 1/8", 1/4", 1/2" and metric 3mm, 4mm, 6mm, 12mm), custom included angles (15°, 20°, 30°, 45°, 60°, 90°), and custom tip flats (0.05mm to 3.0mm) built to your exact manufacturing drawings.
Compare cutter geometries, material suitability, speed/feed parameters, and expected tool life for optimal OEM specification.
| Tool Geometry Class | Primary Target Materials | Optimal RPM Range | Feed Rate (mm/min) | Coolant Strategy | Relative Tool Life |
|---|---|---|---|---|---|
| Solid Carbide Flat Bottom V-Bit | Brass, Copper, Aluminum, Soft Steels, Acrylic | 18,000 - 36,000 RPM | 600 - 1,800 mm/min | MQL / Air Blast | Baseline (1.0x) |
| Single Flute DLC Coated Router | Aluminum, Plastics, Carbon Fiber Composite | 24,000 - 45,000 RPM | 1,200 - 3,500 mm/min | Dry / Air Blast | High (3.5x) |
| PCD Diamond Carving Router Bit | Granite, Marble, Engineered Stone, Ceramics | 8,000 - 18,000 RPM | 400 - 1,200 mm/min | Water Flood / Coolant | Ultra High (35x - 50x) |
| ROFE Clad Diamond Cone Bit | Hard Granite, Basalt, Monumental Masonry | 6,000 - 14,000 RPM | 300 - 900 mm/min | Water Flood Required | Extreme (40x - 60x) |
| Micro End Mill (0.2mm - 0.6mm) | PCB FR4, Surgical Stainless, Fine Jewelry Gold | 30,000 - 60,000 RPM | 150 - 500 mm/min | Mist / MQL Spray | Precision-Limited (2.0x) |
| 1/2" Shank Raised Panel Ogee | Hardwoods, Softwoods, MDF, Veneer Panels | 12,000 - 18,000 RPM | 2,000 - 5,000 mm/min | Dust Extraction | High Production (5.0x) |
Combining nearly four decades of tool grinding experience with modern 5-axis CNC grinding precision and rigorous quality inspection protocols.
Our application engineers evaluate your workpiece material, spindle constraints, and cycle time targets to craft optimized custom tool drawings. We welcome modifications to helix angles, relief clearances, and land widths.
Every production batch undergoes Zoller Genius 3 non-contact optical inspection to verify tip radius, included angle, concentricity, and flute symmetry before dispatch. Complete material test certificates (MTC) supplied upon request.
Streamlined international freight support with DDP (Delivered Duty Paid) options straight to UK machine shop facilities. Real-time technical support alignment across UK business hours (GMT/BST).
Direct answers to the most common questions raised by British engineering buyers, toolroom managers, and CNC machine operators.
Standard prototype samples of custom geometry tungsten carbide or PCD bits are ground and inspected within 7 to 10 working days. Express air freight to major UK engineering centers (London, Birmingham, Manchester, Glasgow) typically takes 3 to 5 business days with full tracking and customs clearance support.
Solid carbide V-bits are economical for soft stones like limestone, sandstone, or soft marble. However, for hard UK granite (e.g., Cornish or Scottish granite) or high-volume memorial carving, PCD diamond bits (or ROFE clad diamond cone bits) are strongly recommended. PCD offers up to 50 times longer wear resistance, drastically reducing tool change downtime and dimensional drift.
Yes. We supply both standard metric shanks (3mm, 3.175mm [1/8"], 4mm, 6mm, 8mm, 12mm) and imperial shanks (1/8", 1/4", 3/8", 1/2"). We can also grind custom shank tolerances (e.g., h6 precision shank fit) for high-speed hydraulic or shrink-fit toolholders used in advanced CNC centers.
For non-ferrous materials like aluminum 6082/7075 and copper, we recommend our specialized Colorful PVD Coating or DLC (Diamond-Like Carbon) single flute cutters. These feature a friction coefficient below 0.1, preventing material built-up edge (BUE) and chip welding even when operating under dry air-blast conditions.
Our production facility operates under ISO 9001:2015 quality management guidelines. Micro engraving bits feature tip radius tolerances down to ±0.002mm and included angle accuracy within ±0.25°. Every batch includes optical inspection reports from Zoller measurement systems.
We execute formal Non-Disclosure Agreements (NDAs) prior to reviewing proprietary drawings. Your custom tool geometry, part marking requests, and custom packaging designs remain strictly confidential to your organization.
Contact our application engineering team today. Share your workpiece material, blueprint specs, or target part numbers to receive technical advice, speed/feed recommendations, and wholesale OEM pricing for UK delivery.