
Rock River Tool, Inc.Precision Cutting Tools
Technical Support(800) 345-8924
Talk to an Engineer Explore our premium grade cutting tools engineered with micron-level expansion mechanisms, micro-grain solid carbide tips, and anti-chatter geometry built for demanding metallic workpieces.
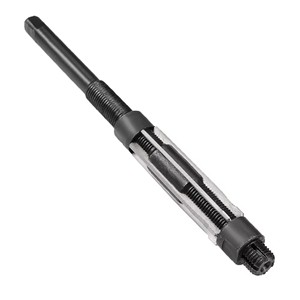
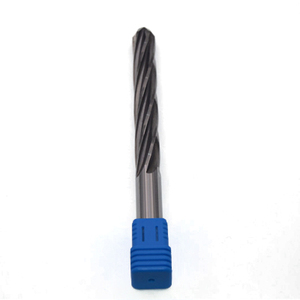
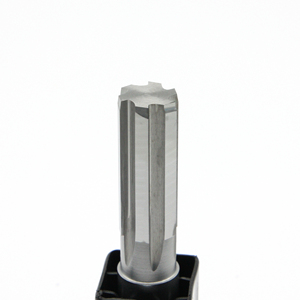
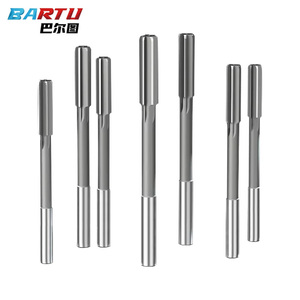

In high-precision mechanical engineering and hole-finishing operations, achieving exacting cylindrical tolerances (such as ISO H6, H7, or H8 limits) presents significant challenges when utilizing fixed-diameter tools. Thermal expansion, spindle deflection, tool wear, and material elasticity frequently cause undersized or out-of-round bores. As China’s premier manufacturer of high-performance cutting tools supplied directly to industrial buyers across Uzbekistan, our engineering design focuses on overcoming these variables through micro-adjustable expansion blade geometry and premium tungsten carbide tipping technology.
An adjustable hand or machine reamer operates via a precision-threaded central arbor featuring ground taper slots. Custom high-speed steel (HSS-M2, HSS-M35 Cobalt) or carbide-tipped blades rest inside these ground slots, secured by dual micro-locking adjustment nuts. By rotating the nuts, the operator smoothly glides the blades along the tapered body, expanding or contracting the tool's effective cutting diameter over a defined range (typically spanning 0.8mm to 3.2mm per tool model across standard H4 to H14 size codes). This mechanical adjustment allows machinists to compensate for edge wear, dial in exact interference fit tolerances for press-fit bearings, and finish non-standard hole sizes without maintaining costly custom tool inventories.
Information Gain Insight: Unlike standard solid reamers that require complete replacement once cutting margins wear down by 0.010mm, our adjustable blade architecture permits up to 15 re-grind and re-expansion cycles. This extends functional tool lifespan by over 350% in high-volume repair workshops and production lines.
Selecting the optimal cutting material and coating substrate is paramount to controlling chatter, achieving surface roughness values down to Ra 0.2 microns, and avoiding catastrophic edge chipping during reaming operations. Our factory categorizes tooling substrates into three specialized performance tiers engineered for distinct workpiece alloys:
| Tool Material / Grade | Substrate Composition | Recommended Workpiece Materials | Target Surface Finish (Ra) | Recommended Speed (SFM) |
|---|---|---|---|---|
| HSS-M35 Cobalt (5%) | High-Speed Steel with 5% Co (HRC 65-67) | Medium Carbon Steels, Structural Steel, Cast Iron | 0.8 – 1.2 µm | 30 – 50 SFM |
| C-2 Grade Carbide (883) | Micro-Grain Tungsten Carbide + 6% Co | Grey Iron, Ductile Iron, Brass, Bronze, Aluminum Alloys | 0.4 – 0.8 µm | 80 – 150 SFM |
| C-5 / C-6 Grade Carbide (370) | TiC-TaC-WC Alloyed Cemented Carbide | Alloy Steels, Tool Steels (P20, D2), Stainless Steel (304/316) | 0.2 – 0.6 µm | 60 – 120 SFM |
| PCD Tipped (Diamond) | Polycrystalline Diamond Layer on Carbide Body | High-Silicon Aluminum, Composites, Copper Alloys | 0.1 – 0.3 µm | 200 – 450 SFM |
Uzbekistan’s rapid economic modernising under the national development policy has catalyzed unprecedented growth across manufacturing, automotive assembly, mineral extraction, and agricultural infrastructure. Delivering localized tool geometry tuned to regional machinery and material stocks is key to our leadership as China's premier reamer exporter into Uzbekistan.
In Tashkent's dense automotive clusters (supplying engine and drivetrain parts for local vehicle manufacturing plants like UzAuto Motors), our PCD and solid carbide machine reamers are heavily deployed for fine-boring engine block cylinder head wrist-pin bushings, aluminum transmission valve bodies, and steering knuckle housings. The high thermal resistance of our bronze-coated spiral flute reamers ensures zero thermal expansion distortion during multi-shift continuous production lines.
The vast open-pit copper, gold, and mineral extraction complexes operated by NGMK (Navoi Mining and Metallurgy Combinat) and AGMK (Almalyk Mining and Metallurgy Combinat) demand extreme-duty tooling. Heavy hydraulic excavators, slurry pumps, and haul truck suspension linkages undergo harsh impact wear. Our H10 to H14 heavy-duty adjustable hand reamer sets allow field maintenance crews in Navoi to perform on-site reboring of worn pivot pin sleeves and boom arm bushings without dismounting massive structural weldments.
Agricultural equipment workshops across Andijan, Namangan, and Fergana require versatile, cost-effective reboring tools for tractor hydraulic control valve sleeves, planetary gear carriers, and cotton harvester spindle gearboxes. Our 11-Piece HSS Adjustable Hand Reamer Sets (spanning 15/32" to 1-1/2") provide maintenance technicians with instantaneous adaptability across metric and imperial non-standard shaft sizes.
Gas processing units and pipeline compressor stations throughout Bukhara and Kashkadarya regions rely on our custom carbide-tipped chucking reamers for reaming heat exchanger tube sheets, high-pressure valve seats, and pump flange bolt holes. The brazed alloy steel body design absorbs high machine vibration while maintaining true circularity on stainless steel and duplex alloys.
Under the "Uzbekistan - 2030" Strategy, the national industrial sector is experiencing a major technological upgrade. Traditional manual conventional lathes and radial drilling machines across state enterprises are being replaced by high-precision 3-axis and 5-axis CNC machining centers. This shift has fundamentally transformed B2B buyer demands for cutting tools within the country:
Combining American engineering heritage (originating from established toolmaking standards) with China's advanced manufacturing scale, we deliver uncompromised tool quality, rapid international dispatch, and dedicated technical service.
Every adjustable blade is ground on 5-axis CNC tool grinders to exact clearance angles and concentricity tolerances, eliminating radial runout and ensuring equal cutting load across all teeth.
Our carbide-tipped reamers utilize high-frequency silver-copper induction brazing techniques. This guarantees maximum joint shear strength between the solid carbide tip and alloy steel body, preventing tip detachment under shock loads.
We manufacture non-catalogue diameters, step reamers, pilot combination tools, and custom shank styles (Morse taper, Weldon flat, straight cylindrical) built precisely to customer CAD drawings within 7-10 business days.
Protect cutting margins with specialized surface treatments including AlTiN (for hardened steel up to HRC 60), TiCCN (for anti-galling on aluminum), and Bronze/TiN (for universal wear resistance and visual thermal tracking).
100% of finished tools undergo 3D optical comparator verification, laser micrometer sizing, and dynamic runout testing. Traceable quality certificates are attached to every export shipment sent to Tashkent customs clearance hubs.
We provide comprehensive logistics support including road freight via Khorgos/Alashankou overland transport, express air cargo directly to Tashkent International Airport (TAS), and full TIR Carnet customs documentation handling.
To maximize tool life and prevent premature edge degradation when reaming with adjustable high-speed steel or carbide-tipped tools, operators should adhere to standard engineering speed reduction guidelines. As a baseline rule, reaming speeds should be set to approximately 50% to 66% of the equivalent drilling speed for the same workpiece material, while feed rates should be increased by 200% to 300% to ensure positive tooth engagement without burnishing.
| Workpiece Material Group | Pre-Ream Stock Allowance (Dia. < 12mm) | Pre-Ream Stock Allowance (Dia. > 12mm) | Carbide Reamer Cutting Speed (SFM) | Feed Rate per Tooth (IPT) | Recommended Coolant Medium |
|---|---|---|---|---|---|
| Low Carbon Steel (< 200 HB) | 0.15 mm – 0.25 mm | 0.30 mm – 0.45 mm | 100 – 140 SFM | 0.003" – 0.006" | Water-Soluble Synthetic Emulsion (8-10%) |
| Alloy / Tool Steel (200-350 HB) | 0.10 mm – 0.20 mm | 0.25 mm – 0.35 mm | 50 – 80 SFM | 0.002" – 0.004" | High-EP Neat Cutting Oil / Heavy Emulsion |
| Grey & Ductile Cast Iron | 0.20 mm – 0.30 mm | 0.40 mm – 0.50 mm | 90 – 130 SFM | 0.004" – 0.008" | Dry with Air Blast or Micro-Drop MQL |
| Aluminum Alloys (< 10% Si) | 0.20 mm – 0.35 mm | 0.45 mm – 0.60 mm | 150 – 250 SFM | 0.004" – 0.008" | Light Soluble Oil / Alcohol-Based Mist |
| Stainless Steel (300/400 Series) | 0.10 mm – 0.18 mm | 0.20 mm – 0.30 mm | 40 – 70 SFM | 0.002" – 0.003" | Sulfurized Heavy Oil with Chlorine Additives |
Get immediate answers regarding ordering protocols, technical specifications, shipping timelines, customs procedures, and custom tool engineering options.
Connect directly with our senior application engineers. Receive detailed CAD tool proposals, material-specific speeds and feeds recommendations, and competitive direct factory pricing within 24 hours.
Get a Quote