
Rock River Tool, Inc.Precision Cutting Tools
Technical Support(800) 345-8924
Talk to an Engineer Engineered for high-volume CNC machining, manual repair line finishing, and micro-tolerance sizing across Malaysian industrial hubs.
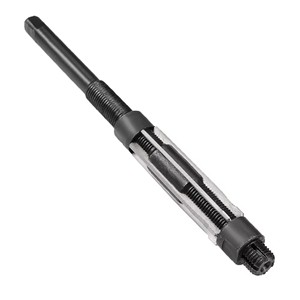
Substrate: Hardened Alloy Steel Body
Adjustment Range: Expandable Micrometer Nuts
Application: On-site Bore Alignment & Repair
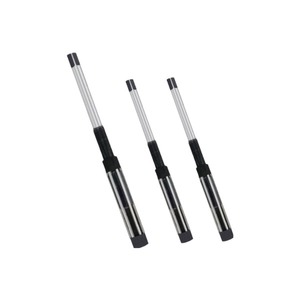
Material: Premium M2 High Speed Steel (HSS)
Blades: 6-Straight Flute Ground Geometry
Finish: Bright Finish / Anti-Corrosion Oil
Feature: Wear-Resistant Blade Guide
Target Bores: Bushing & Bearing Housing Seats
Tolerance: Standard IT8 - IT7 Control
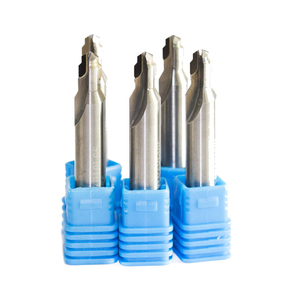
Cutting Tip: Polycrystalline Diamond (PCD)
Machining Target: Aluminum Alloys & Non-Ferrous
Tool Life: Up to 50x vs Standard HSS Tools
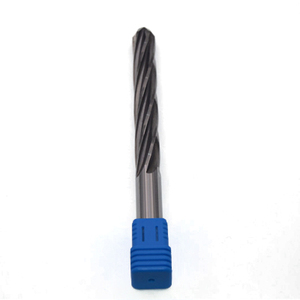
Carbide Grade: Micrograin C2 / C5 Tungsten
Flute Design: Left-Hand Helix / Right-Hand Cut
Surface Hardness: Up to HRC 65 Workpieces
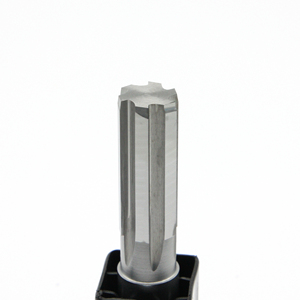
Coating: AlTiN / Bronze Nano-Layer
Flutes: 4-Flute Vibration Damped Spacing
Workpiece: Stainless Steel & Die Steels
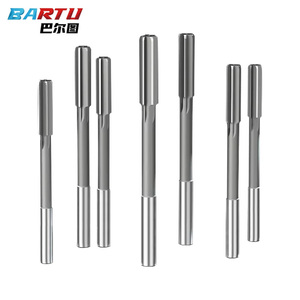
Construction: Brazed Carbide Tip / Steel Body
Teeth: 4 to 6 Tooth Custom Configurations
Advantage: Exceptional Shock & Vibration Absorber

Precision Class: ISO H7 (Micro-inch surface finish)
Shank Type: Straight Shank for CNC Toolholders
Range: Miniature 0.5mm to 12.0mm
Malaysia's industrial sector is undergoing a profound technical evolution driven by the national Industry4WRD framework. As a strategic manufacturing hub in Southeast Asia, Malaysia blends high-tech semiconductor back-end assembly, advanced aerospace component fabrication, precision automotive engineering, and heavy oil & gas equipment manufacturing. Achieving dimensional accuracy down to single-digit micrometers (µm) in cylindrical bores is no longer a luxury—it is a baseline compliance standard.
Adjustable reamers—encompassing expandable hand reamers, carbide-tipped adjustable machine reamers, and PCD (Polycrystalline Diamond) micro-blade reamers—serve as indispensable finishing tools. Unlike fixed-diameter solid reamers, adjustable reamer systems allow production engineers and maintenance technicians to fine-tune bore diameters, compensate for thermal expansion in high-humidity machine shops, and recover tool wear without discarding the cutter body.
Demands ultra-precise PCD and solid carbide adjustable micro-reamers for machining lead frames, aluminum heatsinks, hard disk drive enclosures, and semiconductor automated test equipment (ATE) fixtures requiring Ra < 0.4 µm surface finish.
Requires heavy-duty HSS and carbide-tipped adjustable hand/machine reamers for re-sizing engine valve guides, gearbox housing dowel pin alignment holes, and hydraulic pump block sleeves during Tier-1 OEM manufacturing and aftermarket overhaul.
Focuses on high-rigidity straight-shank carbide reamers and custom multi-stepped adjustable tools designed for machining heat-treated alloy steels, titanium aero-engine brackets, and oilfield control valve bodies.
Selecting the optimal adjustable reamer requires an in-depth understanding of cutter architecture, blade locking mechanics, and substrate compatibility. Our manufacturing facility combines legacy American metal-cutting craftsmanship (established 1986) with modern CNC grinding technology to engineer tools optimized for interrupted cuts, deep bores, and sticky non-ferrous alloys.
| Substrate / Cutting Material | Recommended Workpiece Materials | Max Cutting Speed (SFM / m/min) | Tool Wear Life Index | Primary Malaysian Application Scenario |
|---|---|---|---|---|
| M2 / M35 High Speed Steel (HSS) | Mild Steel (ST37), Carbon Steel, Brass, Soft Cast Iron | 40 - 80 SFM (12 - 25 m/min) | 1.0x (Baseline Standard) | Maintenance repair shops, jig & fixture fitting, educational labs |
| C2 Grade Tungsten Carbide (883) | Cast Iron, 6000/7000 Series Aluminum, Copper, Plastics | 150 - 350 SFM (45 - 110 m/min) | 8.5x vs HSS | Penang electronics housing lines, automotive pump castings |
| C5/C6 Grade Carbide (370) | Alloy Steels (4140/4340), Stainless Steels (304/316L), Tool Steel | 100 - 250 SFM (30 - 75 m/min) | 10.0x vs HSS | High-pressure hydraulic manifold blocks, oilfield valve sleeves |
| Polycrystalline Diamond (PCD) | High-Silicon Aluminum (A380), Carbon Fiber (CFRP), MMC Alloys | 500 - 1500 SFM (150 - 450 m/min) | 40.0x to 60.0x vs HSS | Automotive transmission covers, aerospace composite panels |
A frequent challenge faced by Malaysian CNC machine operators is bore chatter when reaming holes with keyways, cross-drilled oil passages, or split seams. Standard evenly-spaced flute reamers tend to drop into keyways, causing edge chipping and elliptical hole deformation. Our factory solves this by engineering unequal flute spacing (staggered pitch geometry) combined with left-hand spiral flutes that push chips forward in through-holes, maintaining continuous 3-point cylindrical contact.
Transitioning toward sustainable, high-efficiency manufacturing in Malaysia requires strict adherence to material-specific cutting parameters, coolant strategies, and tool preservation protocols adapted for tropical humidity.
When reaming aluminum 6061/7075 in Penang facilities, Minimum Quantity Lubrication (MQL) with synthetic ester oil prevents built-up edge (BUE) on carbide blades. For stainless steel, high-pressure 70-bar coolant delivered through internal channels flushes stringy swarf seamlessly.
Leaving inappropriate pre-reaming stock leads to rapid wear or burnishing. Always leave 0.20mm to 0.38mm (0.008" - 0.015") on diameter for holes under 25mm, ensuring the cutting edge bites into fresh metal rather than rubbing against work-hardened surfaces.
All export shipments to Malaysia are treated with VCI (Vapor Corrosion Inhibitor) oil dipping and vacuum-sealed foil packing. This guarantees that ground HSS and carbide blades arrive 100% rust-free, resisting sea-freight moisture and high ambient humidity.
Below is an empirical feed and speed starting table derived from 38+ years of field testing across aerospace, automotive, and general engineering machine shops:
| Workpiece Material | Hardness (HB/HRC) | Carbide Tipped SFM (m/min) | Feed Rate (mm/rev for Ø10mm-Ø20mm) | Recommended Coolant |
|---|---|---|---|---|
| Free-Machining Carbon Steel (12L14) | 120 - 180 HB | 180 - 250 SFM (55 - 75 m/min) | 0.15 - 0.30 mm/rev | 6% - 8% Water-Soluble Emulsion |
| Alloy Steel (AISI 4140 Annealed) | 180 - 240 HB | 120 - 160 SFM (35 - 50 m/min) | 0.10 - 0.22 mm/rev | Semi-Synthetic Coolant with EP Additives |
| Austenitic Stainless (SS 304 / 316) | 160 - 220 HB | 80 - 120 SFM (25 - 35 m/min) | 0.08 - 0.18 mm/rev | Neat Cutting Oil or High-Pressure 10% Emulsion |
| Cast Iron (Ductile / Nodular) | 160 - 260 HB | 150 - 220 SFM (45 - 65 m/min) | 0.20 - 0.40 mm/rev | Dry with Air Blast or Micro-Emulsion |
| Wrought Aluminum (Al6061-T6) | 80 - 120 HB | 300 - 600 SFM (90 - 180 m/min) | 0.25 - 0.50 mm/rev | MQL Ester Oil or 5% Synthetic Coolant |
As a global tool cutter manufacturer operating continuously since 1986, our enterprise bridges American precision grinding standards with direct B2B export support tailored for Malaysian manufacturing procurement teams. We maintain absolute control over every stage of production—from raw tungsten carbide powder blending to final optical profilometer inspection.
Send us your engineering drawings (CAD/PDF). Our tooling engineers evaluate flute geometry, shank tolerances (h6/h7), and step transitions within 24 hours, ensuring manufacturability before production begins.
Silver-copper induction brazing guarantees high shear strength between carbide blades and steel bodies, eliminating blade slippage under heavy rotational torque in tough alloy steels.
Options include TiAlN for high-temp steel reaming, DLC (Diamond-Like Carbon) for non-ferrous anti-galling, and Bronze AlTiN for extreme abrasive wear resistance on CNC machining centers.
Answers to common technical, commercial, and logistical questions raised by Malaysian machine shop managers, procurement officers, and distributor networks.