MADE IN USA  Carbide Tipped & Solid Carbide Cutting Tools — manufacturing since 1986
Mon–Fri 7:00am–5:30pm CDT · (800) 345-8924

Top Trusted Machine Tap Factories & Supplier

Global B2B Procurement White Paper & High-Precision Threading Technology Guide

High-Performance Machine Taps & Industrial Tapping Systems

Precision-engineered machine taps, form taps, and electric tapping systems manufactured to DIN, JIS, and ANSI industrial standards for high-load production environments.
Metal Electric Tapping Machine M6-M30

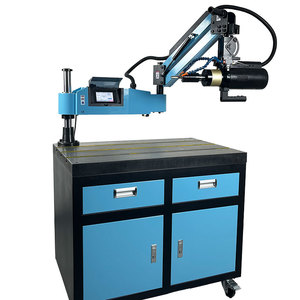
M6-M30 Precision Metal Electric Tapping Machine

  • Capacities: M6 to M30 Metric Threads
  • Feature: Integrated Auto-Lubrication System
  • Control: HD Touchscreen Torque Control
  • Drive: Servo Motor Heavy Duty Head
Send an Inquiry
HSS Cobalt 5% TiN Machine Tap

Amony HSS Cobalt 5% TiN Coated Machine Taps

  • Substrate: M35 HSS-Co (5% Cobalt)
  • Coating: Titanium Nitride (TiN) PVD
  • Geometry: Spiral Flute / Spiral Point
  • Application: Alloy Steels & Stainless
Send an Inquiry
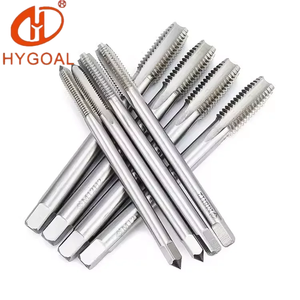
HYGOAL Custom HSS Straight Flute Machine Tap

HYGOAL OEM Custom HSS Straight Flute Machine Tap

  • Substrate: Premium HSS / HSSE
  • Type: Straight Flute Metric Screw Tap
  • Target Materials: Cast Iron & Carbon Steel
  • Tolerance: ISO 2 (6H) Precision Class
Send an Inquiry
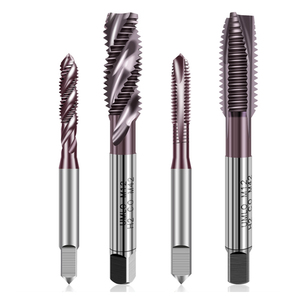
Nano Purple Coated HSSE M42 Machine Tap

Nano-Purple Coated HSSE-M42 Spiral Tip Tap

  • Material: HSSE-M42 (8% Cobalt Grade)
  • Coating: Multi-layer Nano-Purple PVD
  • Range: M2 to M18 High-Speed Taps
  • Specialty: 316/304 Stainless Steel
Send an Inquiry
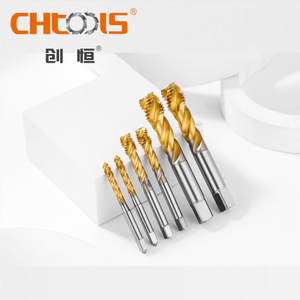
HSS-E JIS Standard TiN Coated Machine Tap

HSS-E Cobalt JIS TiN Coated Spiral Groove Tap

  • Standard: JIS Standard Specification
  • Groove: Helical Spiral Groove Flute
  • Surface: TiN Gold Wear-Resistant Coating
  • Performance: Deep Blind Hole Tapping
Send an Inquiry
Grewin Tools DIN 371 HSS Cobalt Tap

Grewin Tools DIN 371 HSS Cobalt TiAlN Machine Tap

  • Standard: European DIN 371 Dimensional
  • Coating: Titanium Aluminum Nitride (TiAlN)
  • Warranty: 6 Months Industrial Quality
  • Size: M8 Precision Threading Tap
Send an Inquiry
HSS Inch Taper Pipe Thread Machine Tap NPT NPTF

HSS Inch Taper Pipe Thread Machine Tap (NPT/NPTF)

  • Thread Form: NPT, NPTF, G, PT, BSPT
  • Size Range: 1/8" to 7/8" Inch Sizes
  • Material: Ground-from-Solid HSS
  • Use Case: Leak-Tight Pressure Pipe Joints
Send an Inquiry
TiN Coated HSSE Roll Machine Form Tap

TiN Coated HSSE High Performance Roll Form Tap

  • Technology: Chipless Cold Thread Forming
  • Substrate: Premium HSSE Micro-grain Steel
  • Benefits: Zero Chips, 100% Thread Strength
  • Suitability: Ductile Steels & Aluminum
Send an Inquiry
38+
Years Manufacturing Excellence
ISO 9001
Certified Quality Management
60+
Export Destination Countries
0.002mm
Grinding Runout Precision

Enterprise Technical Advantages & Production Competence

Why leading global OEMs, automotive tier-1 suppliers, and aerospace contract manufacturers rely on our high-speed steel and solid carbide threading technologies.

Advanced Metallurgical Formulations

We source premium European and Japanese raw high-speed steel stocks including HSS-E (M35 with 5% Cobalt), HSSE-M42 (8% Cobalt), and ultra-fine tungsten carbide grades (C2/C5/C6). This guarantees extreme hot hardness, grain structure integrity, and exceptional resistance to flank wear under severe thermal cutting stresses.

Proprietary PVD Surface Engineering

Utilizing state-of-the-art Physical Vapor Deposition (PVD) coating chambers, our machine taps feature specialized chemical surface barrier layers: Titanium Nitride (TiN), Titanium Aluminum Nitride (TiAlN), and next-generation Nano-Purple Multi-layer coatings. Surface hardness levels reach up to 3,300 HV with friction coefficients below 0.25.

Rigorous Optical & 3D QA Inspection

Every batch of machine taps undergoes strict quality assurance using 5-axis CNC laser measuring machines and optical profilometers. We inspect major diameter, pitch diameter over-pins, spiral rake angles, relief angles, and thread lead accuracy to verify strict adherence to DIN 371/376, ISO 2 (6H), and JIS standard limits.

Machine Tap Metallurgy & Geometry Selection Guide

Engineering breakdown of tap flute geometries, substrate pairings, and surface treatments optimized for specific workpiece materials and cutting speeds.

Technical Insight: Machine tapping performance is driven by the interaction between chip evacuation dynamics, mechanical rake angle, and surface lubricity. Selecting an improper flute geometry for blind vs. through-hole applications accounts for over 70% of premature tap breakage in automated CNC centers.

Tap Flute Geometry Evacuation Direction Recommended Hole Type Optimal Workpiece Material Cutting Speed (SFM) Recommended Surface Coating
Spiral Point (Gun Tap) Pushes chips forward (Ahead of tap) Through Holes (1.5D to 3D depth) Carbon Steels, Structural Steel, Aluminum 45 – 90 SFM TiN Gold
Spiral Flute (35° - 45° Helical) Pulls chips upward (Out of shank) Blind Holes (Up to 2.5D depth) Stainless Steels (304/316), Alloy Steels 30 – 65 SFM Nano-Purple / TiAlN
Straight Flute Stores chips inside flutes Shallow Blind / Cast Iron Through Holes Gray Cast Iron, Ductile Iron, Brass 25 – 50 SFM Steam Oxide / Bright
Cold Forming (Roll Tap) Chipless (Material Displacement) Through & Blind Holes (Ductile Materials) Aluminum Alloys, Soft Copper, Low Carbon Steel 60 – 120 SFM TiN / TiCN
NPT / NPTF Pipe Tap Radial evacuation along taper Tapered Pipe Thread Holes Pressure Manifolds, Valve Bodies, Castings 20 – 40 SFM TiAlN / Oxide

Future Machine Tap Procurement Trends & Industry Outlook (2025–2030)

Key technological and market shifts driving international B2B buyers toward advanced machine tap suppliers and smart tapping equipment.

1. Transition to High-Speed MQL Tapping

With environmental regulations restricting flood coolants, industrial manufacturers are shifting toward Minimum Quantity Lubrication (MQL). Machine tap manufacturers are engineering multi-layer micro-thin coatings (AlTiN/DLC) and custom micro-chipping edge preparations specifically designed to reduce thermal friction under near-dry cutting conditions.

2. Surge in Chipless Cold Form Threading

Automotive EV lightweighting initiatives have accelerated the adoption of aluminum structural castings. Cold forming (roll) taps are rapidly replacing traditional cutting taps due to their ability to produce 100% chip-free operations, higher thread shear strength (by 15-20%), and significantly extended tool fatigue resistance.

3. Adoption of Servo-Driven Torque Control

The global market for electric tapping machines is expanding rapidly. Modern M6-M30 servo-driven electric arms with real-time torque feedback prevent tap breakage in expensive large castings by instantly reversing rotation upon detecting localized metal hardness spikes or blind hole bottom contact.

Frequently Asked Questions for B2B Tap Procurement

Technical guidance and answers to common questions raised by procurement managers, tooling engineers, and machine shop buyers.

What is the critical difference between Spiral Point (Gun Taps) and Spiral Flute Machine Taps?
Spiral Point (Gun) Taps feature an angular cutting face ground into the first few threads that forces chips ahead of the tap direction. They are specifically designed for through holes. In contrast, Spiral Flute Taps have helical flutes (typically 35° or 45°) that draw continuous stringy chips upward toward the shank, making them mandatory for blind holes to prevent chip packing and catastrophic tap breakage at the bottom of the hole.
When should buyers select HSSE-M42 (8% Cobalt) over standard HSS-M2 machine taps?
HSSE-M42 contains 8% Cobalt substrate alloy, offering exceptional red-hardness (ability to maintain cutting edge sharpness up to 600°C/1100°F). Buyers should specify M42 taps when machining tough, work-hardening alloys such as AISI 316 stainless steel, Inconel 718, titanium, or structural steels with tensile strength exceeding 900 MPa. For standard low-carbon steels and easy-machining metals, HSS-M2 or M35 (5% Cobalt) remains the cost-effective choice.
How does pre-tap hole sizing differ between Cut Taps and Forming (Roll) Taps?
Cutting taps slice away metal to form the internal thread profile, requiring a standard pre-drilled pilot hole calculated as: Drill Diameter = Nominal Tap Diameter - Pitch. Forming taps do not remove metal; instead, they plastically displace material into the tap's thread peaks. Consequently, Form Taps require a significantly larger pre-drilled hole size. Using a cut-tap pre-drill size for a form tap will result in extreme torque over-loads and immediate tap destruction.
What thread tolerance classes (6H, 2B, JIS 2) should we specify on OEM technical drawings?
Tolerance specification depends on regional and industry requirements. ISO 2 (6H) is the international metric standard corresponding to standard commercial fits for metric fasteners. ANSI 2B is the standard class for Unified Inch threads (UNC/UNF). JIS 2 is the traditional Japanese standard. If parts are slated for electroplating or heat treatment after tapping, procurement should request oversize taps (e.g., 6G or +0.03mm oversize) to compensate for plating thickness buildup.
Can your factory provide custom special machine taps based on component drawings?
Yes. Our manufacturing facilities specialize in OEM/ODM custom thread tap manufacturing. We engineer modified shanks (Morse taper, Weldon flat, extended reach), special chamfer leads (1.5P short chamfers for tight blind hole clearances), non-standard thread pitches, combined drill-and-tap step tooling, and custom PVD coating stacks. Send your technical CAD/PDF drawings for an engineering manufacturability review and fast price quote.
What advantage does an integrated electric tapping machine offer over CNC machining center tapping?
While CNC machining centers excel at high-speed milling and drilling, tying up expensive 5-axis or 3-axis CNC spindles for secondary tapping operations is cost-inefficient. Portable or station-mounted electric tapping machines (M6-M30) equipped with flexible articulated arms allow operators to tap large, heavy workpieces or multiple off-axis holes rapidly while freeing up CNC spindle time. Integrated torque-limiting chucks also drop tap breakage rates to near zero.

Partner with a World-Class Machine Tap Manufacturer

Need custom tool geometry, high-volume B2B wholesale pricing, or technical selection assistance for difficult-to-machine alloys? Contact our tooling engineers today.

Send an Inquiry