Rock River Tool, Inc.Precision Cutting Tools
Technical Support(800) 345-8924
Talk to an Engineer Explore our certified range of high-speed steel (HSS), Cobalt, and solid carbide rotary tools. Engineered for micro-hole tolerances, high thermal resistance, and extended tool life across CNC machining operations.





An authoritative analysis for procurement officers, tooling engineers, and manufacturing executives evaluating Chinese OEM/ODM suppliers for step drills, machine reamers, and custom multi-flute cutting tools.
Leading Chinese manufacturers have modernized material procurement by utilizing micro-grain tungsten carbide (grain size 0.4μm–0.6μm) and cobalt-alloyed high-speed steel (HSS-Co M35 / M42). This transition ensures superior edge toughness, resisting micro-chipping during high-speed step drilling into structural steel, stainless sheet metal, and aerospace alloys.
To withstand extreme friction heat during multi-stage drilling without coolant, modern Chinese step drill suppliers employ Physical Vapor Deposition (PVD) surface treatments. Multi-layer coatings like TiAlN (Titanium Aluminum Nitride), AlTiSiN, and DLC (Diamond-Like Carbon) raise surface micro-hardness above 3200 HV while lowering friction coefficients down to 0.2.
Achieving H7/H8 hole tolerance across sequential diameter steps requires state-of-the-art grinding kinematics. Top-tier manufacturers employ 5-axis Rollomatic, ANCA, and Walter CNC grinders equipped with laser radial runout compensation, delivering pitch concentricity within 0.003 mm for vibration-free hole expansion.
Combining decades of tooling legacy, specialized CNC grinding technology, and strict quality control protocols to supply high-reliability step drills, machine reamers, and custom profile cutters.
While solid carbide step drills deliver maximum rigidity for high-RPM machining centers, brazed carbide-tipped designs provide an ideal middle ground for large-diameter hole expansion and interrupted cuts. By brazing premium micro-grain carbide teeth onto tough, alloy steel tool bodies, our suppliers deliver exceptional impact absorption alongside extreme wear resistance.
Step drills eliminate multiple tool changes by enabling single-pass drilling, deburring, and chamfering. Leading Chinese producers utilize CAD/CAM simulation software to customize step angles (90°, 118°, 135°, or custom countersink steps) and flute profiles (Straight Flute, Spiral Flute, or Dual-Spiral Flute) tailored specifically for your target metal substrate.
Understanding technology shifts empowers engineering teams and buyer organizations to optimize tooling life, reduce cycle times, and select suppliers aligned with future manufacturing standards.
Deep-hole step drilling and high-speed machine reaming increasingly demand internal through-coolant channels. By delivering high-pressure coolant directly to the cutting edge, internal coolant channels purge chips instantly, prevent thermal shock, and increase cutting speeds (SFM) by up to 40% when machining abrasive cast iron and aerospace alloys.
Future tool designs leverage functionally graded carbide materials. The tool core retains high fracture toughness to absorb torsion stress, while the outer step margins feature ultra-dense micrograin carbide enriched with wear-resistant binder phases. This metallurgy dramatically reduces corner wear on step transitions.
Quality verification in leading Chinese manufacturing plants is moving toward 100% automated optical & laser measurement systems. Non-contact inspection machines verify step diameter pitch, lip clearance angles, and flute rake profiles against CAD models, guaranteeing zero-defect shipments for high-volume automotive & structural orders.
Refer to this empirical data guide when choosing step drill substrates, fluting options, and coating formulations for specific workpiece materials.
| Workpiece Material | Recommended Substrate | Flute Configuration | Optimal Coating | Surface Speed (SFM) | Hole Tolerance Class |
|---|---|---|---|---|---|
| Structural Steel (< 28 HRC) | HSS-Co M35 / Solid Carbide | Spiral Flute (30° Spiral) | TiAlN / Bronze PVD | 80 - 150 SFM | H7 / H8 Precision |
| Stainless Steel (304 / 316) | HSS-Co M42 / Micrograin Carbide | Dual-Spiral Flute | AlTiSiN / TiSiN Nano | 40 - 80 SFM | H7 Precision |
| Cast Iron (Gray & Ductile) | Carbide Tipped / Solid Carbide | Straight Flute | Bronze / Uncoated C2 | 120 - 220 SFM | H7 / H8 Precision |
| Aluminum & Non-Ferrous | Solid Carbide / Premium HSS | Polished Spiral Flute | TiB2 / DLC / Uncoated | 250 - 500 SFM | H7 Precision |
| Thin Sheet Metal / Duct Work | HSS 6542 / M35 | Straight / Spiral Flute | Titanium Nitride (TiN) | 100 - 180 SFM | Standard Step Class |
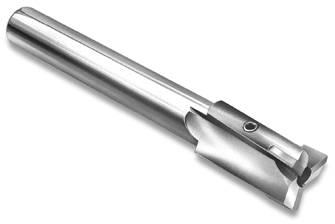
Straight, taper, and capscrew shank counterbores for socket-head fasteners.
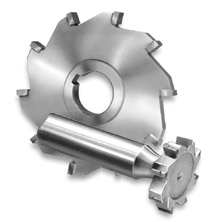
Side milling cutters, slitting saws, and keyseat profile tooling.
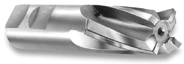
Center-cutting straight and high-spiral shear end mills for metal removal.
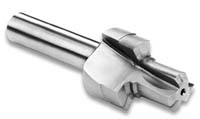
Compliant with SAE MS16142, J514F, J1926, and MS33649 specifications.
Morse, Jarno, and Brown & Sharpe taper lathe centers for precision turning.
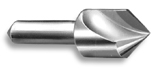
Single flute and three-flute countersinks designed for chatter-free chamfering.
Get direct engineering answers regarding custom step drill fabrication, lead times, quality assurance, and minimum order quantities.
Step drills enable multi-diameter drilling, chamfering, deburring, and counterboring in a single continuous tool pass. This reduces tool-change cycle times on CNC machining centers, prevents sheet metal deformation, eliminates the need for pilot hole punching, and creates cleaner burr-free hole edges compared to standard jobber length twist drills.
Choose Cobalt High-Speed Steel (HSS-Co M35 with 5% Cobalt or M42 with 8% Cobalt) for hand-held drilling, magnetic drill presses, thin sheet metals, structural tubing, and operations where machine rigidity is limited. Choose Solid Carbide or Carbide-Tipped step drills for high-volume CNC automated machining centers where rigidity is high and maximum tool life at elevated surface speeds (SFM) is mandatory.
Yes. Premier Chinese manufacturers specialize in custom OEM/ODM production based on customer CAD prints or technical specifications. You can specify exact step diameters, step lengths, step transition angles (90°, 118°, 135°), flute helix angles, shank profiles (3-flat, hex, straight, or Morse taper), and custom PVD coatings tailored for specific workpiece materials.
Standard precision machine reamers are produced to H7 tolerances (typically within +0.000/-0.012 mm depending on diameter). High-precision custom reamers and step drill diameter steps can be ground to H6 or H7 precision upon request using 5-axis CNC optical grinding centers with full Zoller laser verification certificates.
Standard catalogue tools are typically stocked for immediate dispatch. For customized step drills or non-standard machine reamers, prototype sample production takes 7 to 10 working days. Full volume OEM production orders usually take 15 to 25 days depending on PVD coating batch schedules and quantity requirements.
PVD (Physical Vapor Deposition) coatings such as TiAlN or AlTiSiN create a microscopic ceramic barrier over the cutting edge. This barrier exhibits thermal stability up to 900°C–1100°C, drastically reducing thermal wear, preventing material built-up edge (BUE) when machining sticky alloys, and extending overall tool life by 300% to 500% compared to bright uncoated tools.
Partner directly with leading Chinese tool engineering specialists. Submit your tool drawings, target material specifications, or bulk sourcing requirements to receive competitive factory pricing within 24 hours.