
MADE IN USA  Carbide Tipped & Solid Carbide Cutting Tools — manufacturing since 1986
Mon–Fri 7:00am–5:30pm CDT · (800) 345-8924
Industrial Grade Tooling White Paper 2026

Top China Cutting Tool Manufacturer & Factories

Precision Sub-Micron Carbide Engineering, H7/H8 Tolerance Standards & Global OEM Procurement Intelligence

Precision Machining Reamers & OEM Cutting Solutions

Explore our industrial catalog engineered for high-precision finishing, micro-hole execution, and heavy-duty directional reaming.


Solid Carbide Machine Reamer Bronze Coated
Solid Carbide Machine Reamer 0.5–12.0mm H7 Bronze Coated
Substrate: Sub-Micron Carbide Tolerance: ISO H7 Precision Flute Type: Straight & Spiral Options
Inquire Now
H7 HSS Machine Reamer Deep Hole Hand Reaming Tool
H7/H8 HSS Machine Reamer Deep Hole Tool (55HRC)
Material: Premium M2/M35 HSS Cooling: Dry & Internal Coolant Helix Angle: 15°–20° Shear Cut
Inquire Now
1mm to 20mm Carbide Machine Reamer Coated
1mm to 20mm Carbide Coated Straight Flute H7 Reamer
Diameter Range: 1.0mm – 20.0mm Coating: TiAlN / AlCrN Physical Vapor Target: Alloy Steel & Cast Iron
Inquire Now
Custom High-Speed Steel Machine Reamer Non-Standard
Custom Extended HSS Straight Shank Reamer H7/H8
Customization: Non-Standard Lengths Material Grade: Cobalt High-Speed Steel Application: Aviation & Die Finishing
Inquire Now
Horizontal Directional Drilling Machine Fluted Reamer
Horizontal Directional Drilling (HDD) Machine Fluted Reamer
Duty Grade: Heavy Trenchless Mining Hardfacing: Tungsten Carbide Matrix Compatibility: Major Brand Rig Interfaces
Inquire Now
Straight Shank High Speed Steel Manual Reamer
High-Precision HSS Straight Shank Manual & Metal Reamer
Operation: Manual / Low SFM CNC Chamfer Lead: Long Pilot Entry Chamfer Economics: High ROI Volume Sourcing
Inquire Now
CNC Milling Reamer Carbide Spiral Tool Sets
CNC Spiral Flute Solid Carbide Reamer & Tool Sets
Set Range: Multi-Diameter Precision Kits Helix Angle: 45° High Spiral Cutting Surface Finish: Ra < 0.2 µm Achievable
Inquire Now
Wholesale 20mm Carbide Reamer High Quality Alloy
Industrial Direct Wholesale 20mm Carbide Alloy Machine Reamer
Nominal Diameter: 20.0mm ISO Standard Rigidity: Maximum Heavy Cut Stability OEM Tier: Automotive & Hydraulic Grade
Inquire Now
0.4 µm
Ultra-Fine Sub-Micron Grain
±0.001 mm
H7/H8 Tolerance Control
68 HRC
Max Cut Hardness Capacity
100%
Zoller Laser Metrology Test

1. Substrate Metallurgy & Material Selection Engineering

In modern computer numerical control (CNC) finishing operations, selecting between micro-grain solid tungsten carbide (WC-Co) and cobalt-alloyed high-speed steel (HSS-E/M35) represents a fundamental trade-off between Transverse Rupture Strength (TRS) and Vickers Hardness (HV). As leading Chinese cutting tool manufacturers upgrade their powder metallurgy sintering processes, understanding substrate microstructures is essential for international procurement teams aiming to reduce cost-per-edge while maximizing tool longevity.

Tungsten carbide reamers engineered in top-tier Chinese manufacturing centers employ sub-micron grain sizes ranging from 0.4 µm to 0.8 µm. Bound with an optimized 6% to 12% cobalt matrix, these tools achieve a hardness exceeding 1,600 HV10, making them highly resilient against thermal deformation during dry machining or high-velocity coolant-fed operations. Conversely, HSS-E M35 and M42 reamers, enriched with 5% to 8% Cobalt, deliver superior ductility (TRS > 3,500 MPa), preventing tooth breakage under severe interrupted cuts or non-rigid manual setup conditions.

Information Gain Insights: Sub-micron solid carbide tools operating at surface speeds ($SFM$) 3x to 4x higher than standard HSS require strict TIR (Total Indicated Runout) alignment. A toolholder runout exceeding $0.005 \text{ mm}$ will cause unequal tooth engagement, leading to micro-chipping along the 45° primary chamfer angle.
Substrate Parameter Ultra-Fine Solid Carbide (0.4µm) Co-Alloyed HSS (M35 / H8 Class) Carbide Tipped (Braze Bonded)
Vickers Hardness (HV30) 1,650 – 1,850 HV 850 – 950 HV 1,500 – 1,700 HV (Tip Only)
Transverse Rupture Strength (TRS) 3,800 N/mm² 4,200 N/mm² 2,900 N/mm² (Joint Limited)
Max Workpiece Cut Hardness Up to 68 HRC Up to 38 HRC Up to 55 HRC
Thermal Stability Threshold 1,100 °C 600 °C 850 °C (Braze Thermal Limit)
Ideal Machining Environment High-Rigidity CNC, Internal Coolant Manual Lathes, Interrupted Bore Cuts Heavy Cast Iron Bore & Valve Seats

Advanced Manufacturing Infrastructure & OEM Expertise

Integrating European 5-axis grinding technology with Chinese raw material supply chain efficiency.

5-Axis CNC Grinding Precision

Utilizing high-precision Walter Helitronic and Rollomatic 5-axis CNC grinding machines to maintain tooth pitch tolerances within ±0.001mm and achieve smooth chip evacuation geometry.

Zoller Laser Metrology Verification

100% of export batch reamers undergo non-contact laser optical inspection on Zoller Genius 3 platforms, generating verifiable inspection reports for helix angle, diameter, and edge hone radii.

Custom PVD/CVD Nanocoating Engine

In-house PVD physical vapor deposition coating chambers deliver Bronze TiAlSiN, AlCrN, and Diamond-Like Carbon (DLC) films to extend tool life across stainless steel, titanium, and abrasive non-ferrous metals.
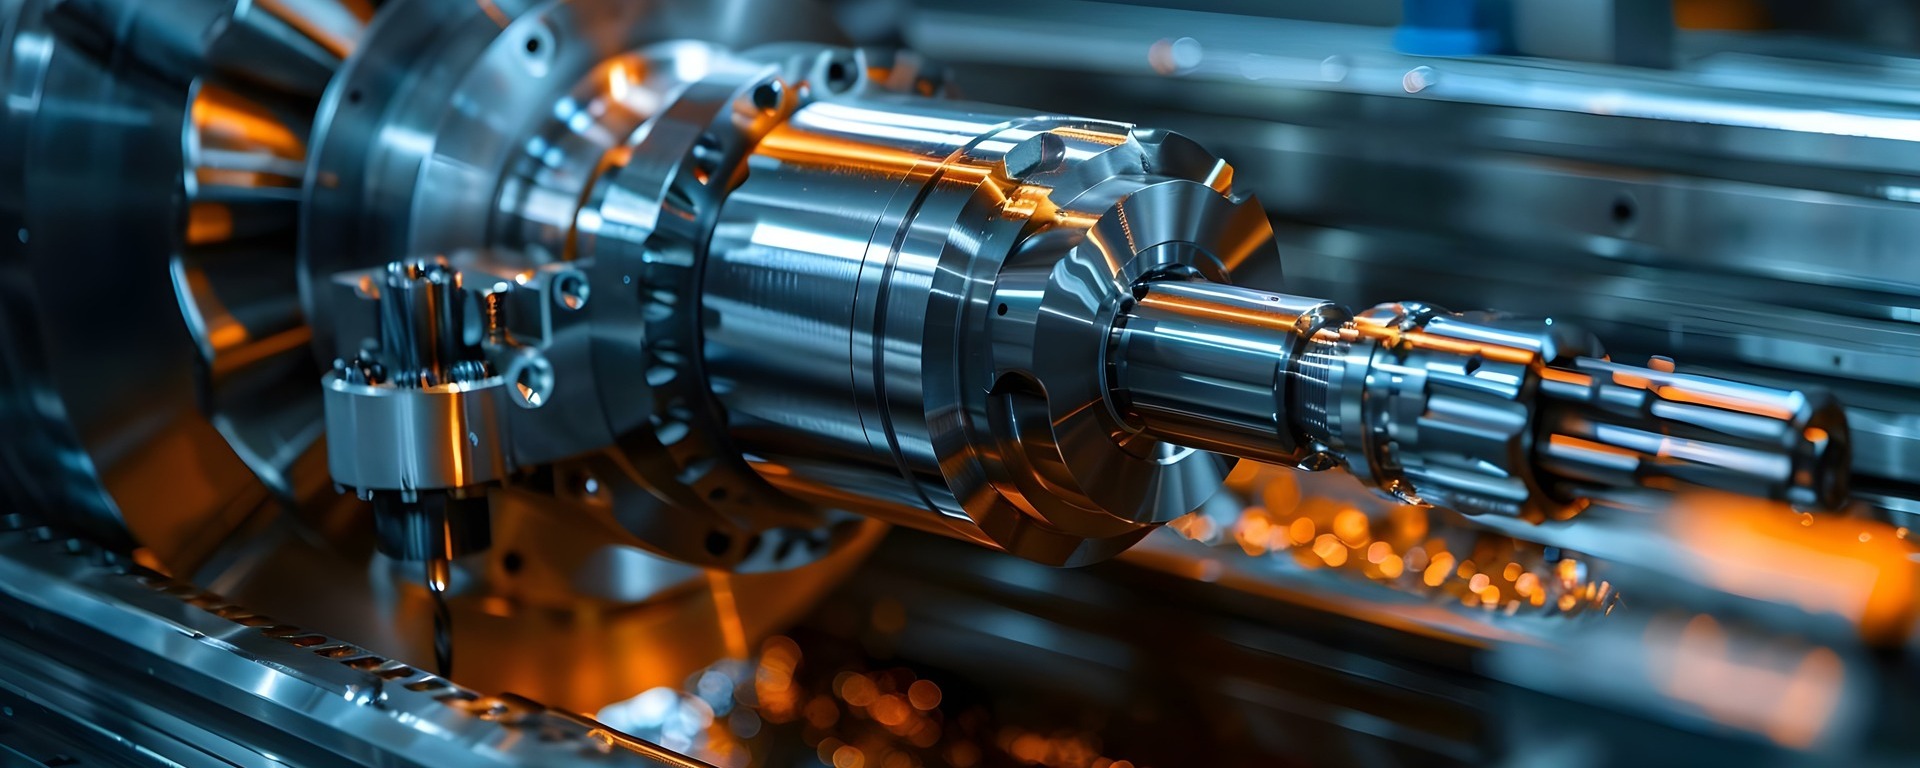
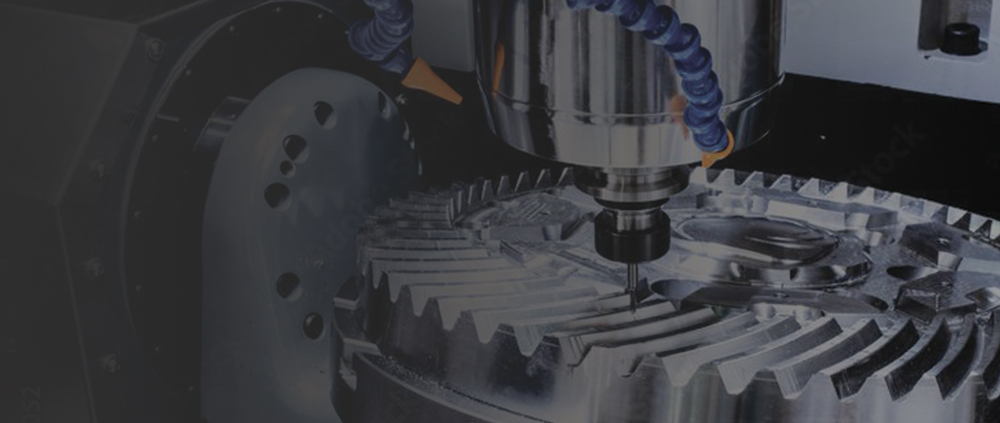
China Advanced Cutting Tool Factory Machining Line

2. Next-Generation Tooling Trends: Nano-Laminated Coatings & Geometry Optimization

The global industrial cutting tool market is undergoing a rapid transition toward high-efficiency, dry, and minimum quantity lubrication (MQL) machining. China's top cutting tool factories are at the forefront of this shift, replacing traditional single-layer TiN or TiC coatings with multi-layered nanostructure PVD coatings.

Trend A: Multi-Flute Asymmetrical Spiral Geometries

Standard straight-flute reamers are increasingly being superseded by unequally spaced asymmetrical spiral flutes (ranging from 15° to 45° helix). This non-uniform tooth pitch eliminates harmonic chatter frequencies during deep-hole finishing, yielding hole roundness tolerance within < 0.002 mm and surface roughness ratings of Ra 0.15 µm.

Trend B: Internal Through-Coolant (Coolant-Fed Reamers)

For blind-hole and deep bore operations, micro internal coolant channels discharging directly at the cutting face flush chips forward or backward efficiently. This eliminates chip recutting—the primary cause of wall scratching and premature fluting wear in nickel-based superalloys.

Furthermore, the adoption of Bronze AlTiSiN (Aluminum Titanium Silicon Nitride) nanocomposite coatings provides a thermal barrier up to 1,200°C. The oxidation of silicon creates an amorphous $SiO_2$ layer that acts as a self-lubricating barrier, preventing built-up edge (BUE) formation when machining gummy materials such as austenitic 316L stainless steel and 6061-T6 aluminum alloys.

3. Comprehensive Tool Category Matrix for B2B Sourcing

Major Chinese manufacturers support diverse tooling portfolios engineered to cover the complete spectrum of metal removal—from heavy slotting to micro-finish reaming.
Carbide Tipped Chucking Reamer
Carbide Tipped Chucking Reamers

Combines shock-absorbing alloy steel shanks with wear-resistant carbide cutting edges. Perfect for cast iron and interrupted cuts.

Inquire Now
Carbide Tipped Jobber Drills
Jobbers & Stub Length Carbide Drills

High-rigidity hole-making tools designed to resist deflection during high-feed drilling into hardened steel dies and structural plates.

Inquire Now
Carbide Tipped Counterbores
Straight & Aircraft Counterbores

Precision-ground pilots ensure concentric countersinking for socket head capscrews and structural aerospace fasteners.

Inquire Now
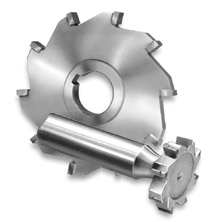
Arbor Hole Slitting Saws and Cutters
Arbor Hole Milling Cutters & Saws

Side milling cutters and slitting saws with tight side-runout control for narrow slotting, parting, and precision keyseat milling.

Inquire Now
High Spiral End Mills
High-Spiral Shear End Mills

Center-cutting solid carbide and carbide-tipped end mills engineered for smooth shear force reduction during high-speed peripheral milling.

Inquire Now
SAE Port Contour Cutters
SAE & MS Port Contour Cutters

Form tools compliant with MS16142, J1926, and MS33649 specs for single-pass hydraulic porting, chamfering, and spotfacing.

Inquire Now

4. Global OEM Procurement Dynamics: China Sourcing Roadmap 2026–2030

As procurement directors re-evaluate global supply chain resilience, Chinese cutting tool factories are shifting from low-cost mass production to high-precision OEM customization. Modern buyers must analyze their suppliers using a Total Cost of Ownership (TCO) model rather than unit purchasing cost alone.

Key strategic shifts in China’s cutting tool manufacturing ecosystem include:
  • Digital Twin Tooling Models: Premium factories provide 3D STEP models and DXF tool geometry data alongside 3D tool wear simulation files to streamline CAM programming for international clients.
  • Consolidated Raw Material Supply: Domestic raw material integrated suppliers (such as Zhuzhou Cemented Carbide Group) ensure raw tungsten ore purity, shielding overseas buyers from global price volatility.
  • Rapid Prototyping & OEM Customization: Non-standard reamers, step drills, and custom form tools can move from CAD drawing approval to finished PVD-coated tools in under 10 business days.
Special Tooling Engineering and Manufacturing Capability

Frequently Asked Questions (B2B Technical FAQ)

Expert engineering answers to common inquiries regarding precision tolerances, stock allowance, and custom tooling orders.

Q1: What pre-drilling stock allowance should be left prior to running an H7 solid carbide reamer?
As a standard engineering practice, leave approximately 0.15 mm to 0.25 mm (0.006 in to 0.010 in) on diameter for holes under 10mm, and 0.25 mm to 0.40 mm (0.010 in to 0.015 in) for diameters up to 20mm. Leaving too little stock causes the reamer teeth to burnish or rub rather than shear, leading to rapid margin wear and work hardening, while excessive stock risks chip jamming and tooth fracture.
Q2: When should I specify a carbide-tipped reamer over a solid carbide reamer?
Carbide-tipped reamers feature a micro-grain tungsten carbide tip brazed onto a tough alloy steel shank. They are recommended for large diameter holes (>12mm), interrupted cuts (such as keyways or cross-holes), cast iron machining, and applications on older CNC equipment with lower dynamic rigidity. The steel body absorbs severe impact loads that could snap solid carbide, while offering a lower cost per tool.
Q3: How does flute helix orientation affect chip evacuation in blind vs. through holes?
For through holes, a left-hand helix with right-hand cutting direction pushes chips forward ahead of the tool, protecting the reamed surface from scratches. For blind holes, a right-hand helix with right-hand cut pulls chips upward out of the hole, preventing chip accumulation at the bottom of the bore. Straight flute reamers remain the standard choice for general-purpose short-bore execution.
Q4: What quality control documentation accompanies wholesale OEM tool orders?
Standard export batches from certified Chinese factories include material batch test reports (SGS/ISO chemistry certification), PVD coating thickness certification, and Zoller optical inspection certificates detailing major/minor diameter tolerances, runout (<0.003mm), and edge hone radii.
Q5: Can tools be customized to match non-standard prints or specialized aerospace standards?
Yes. Our engineering team designs custom tools according to customer drawings (CAD/STEP), supporting non-standard diameters, custom step angles, special pilot lengths, coolant-through configurations, and specialized aerospace port standards (MS16142, MS33649, SAE J1926).
Q6: How do I select between Bronze TiAlN coating and AlCrN coating for stainless steel finishing?
Bronze TiAlN/TiAlSiN provides excellent lubricity and thermal resistance for general stainless steels (304/316) under wet conditions. For high-temperature alloys (Duplex stainless, Inconel 718, Titanium Grade 5), AlCrN (Aluminum Chromium Nitride) is preferred due to its superior micro-hardness (3,200 HV) and extreme resistance to abrasive flank wear during high-speed cuts.
Direct Factory Support

Ready to Optimize Your Cutting Tool Sourcing & Machining Costs?

Send us your part prints, target tolerances, or current tool numbers. Our application engineers provide free manufacturability reviews and competitive OEM quotes within 24 hours.





