
Rock River Tool, Inc.Precision Cutting Tools
Technical Support(800) 345-8924
Talk to an Engineer Engineered for extreme wear resistance, rigid mechanical stability, and high-speed multi-axis CNC machining across aerospace, downhole drilling, and automotive production.
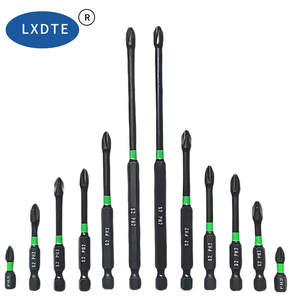
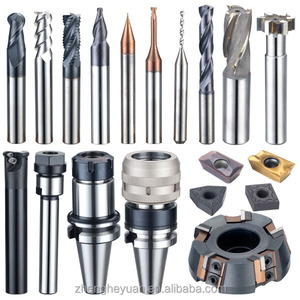
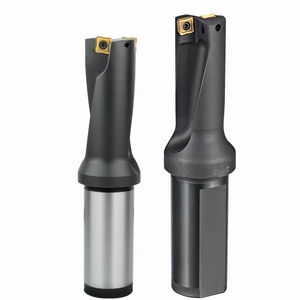
In modern high-speed machining, oilfield exploration, aerospace structural milling, and precision automated assembly, tool bits represent the primary contact interface between machine power and raw workpiece material. Selecting the top global tool bit suppliers and exporters requires a granular understanding of metallurgical composition, physical vapor deposition (PVD) coating performance, shank concentricity, and total cost-per-cut engineering.
Global industrial supply chains demand suppliers capable of maintaining rigorous geometric tolerances under high thermal and mechanical stresses. Whether evaluating S2 alloy steel driver bits subjected to cyclic impact loads or micro-grain tungsten carbide end mills cutting tough heat-resistant superalloys (HRSA), enterprise buyers must look beyond initial unit prices to analyze Information Gain parameters: tool wear rate, chip evacuation geometry, brazing shear strength, and dynamic runout (TIR).
Transitioning from standard HSS steel to sub-micron C-2 (883 grade) tungsten carbide for non-ferrous materials and C5/C6 (370 grade) for steel alloys elevates tool life by 300% to 500%.
Multi-layer AlTiN, TiSiN, and Diamond-like Carbon (DLC) coatings create thermal barriers exceeding 900°C oxidation thresholds, allowing dry machining and reduced MQL consumption.
Leading exporters maintain full batch-level chemical traceability, ISO 9001 certification, laser-interferometer inspection, and strict runout tolerances below 0.005mm TIR.
To assist procurement specialists, tooling engineers, and global distributors, the following comparative framework analyzes the leading global manufacturing hubs and exporter profiles. This data reflects real-world shop-floor performance metrics, custom engineering capabilities, and order fulfillment capabilities.
| Supplier Category / Tier | Primary Substrate Focus | Target Applications | Key Advantage | Customization Support |
|---|---|---|---|---|
| Rock River Tool, Inc. (USA) | Brazed Carbide Tipped & Solid Carbide (C2, C5, C6) | Reaming, Counterboring, Port Cutters, End Mills | Shock-resistant alloy steel body + premium carbide tip | 100% Custom Blueprints & Modification |
| Tier-1 European CNC Manufacturers | Micro-Grain Solid Carbide & PCD | 5-Axis High-Speed Aerospace & Medical | Ultra-tight tolerances (<0.002mm TIR) | High-Volume Standard Catalogs |
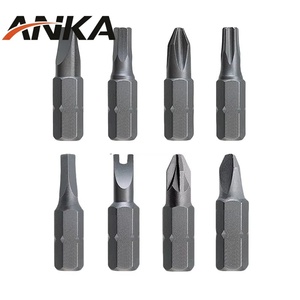
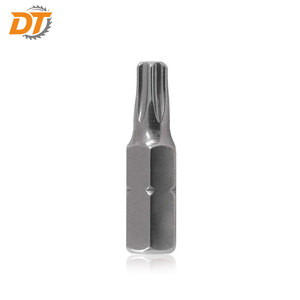
| S2 Screwdriver Bit Exporters (Taiwan/China) | S2 Industrial Tool Steel (HRC 58-62) | Automotive Assembly, Power Impact Driving | Torsion zone energy absorption & high torque | OEM Branding & Packaging |
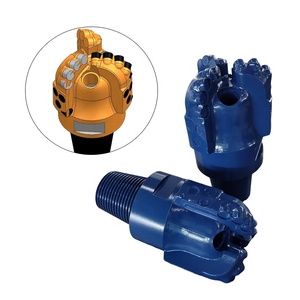
| Downhole Rock Bit Suppliers | PDC Compacts & Tungsten Carbide Matrix | Geothermal, Oil & Gas, Mining Shafts | Extreme erosion and impact resistance | Custom Cutter Layouts |
| Indexable U-Drill Exporters | Hardened Tool Steel Body + Carbide Inserts | Heavy Metal Drilling (Steel & Cast Iron) | Fast chip evacuation via internal coolant channels | Standard ISO Insert Compatibility |
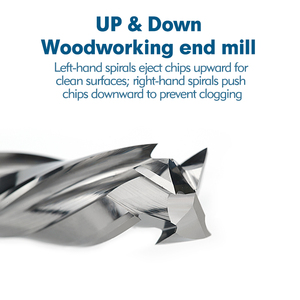
While solid carbide tools provide superior rigidity for high-speed light finishing, brazed carbide tipped tools (pioneered by top domestic manufacturers like Rock River Tool since 1986) combine a resilient alloy steel body with a tungsten carbide cutting edge. This construction absorbs mechanical shock, cross-hole intermissions, and spindle vibration—delivering significantly higher fracture resistance and lower cost-per-hole on diameters exceeding 0.500 inches.
Understanding the wear mechanisms of tool bits requires analyzing the microstructural properties of the three predominant substrate materials supplied by global exporters:
S2 steel is a silicon-manganese tool steel engineered specifically for high-impact applications. Through controlled vacuum heat treatment and precision tempering, S2 bits achieve a surface hardness of HRC 58 to 62 while retaining high core toughness. When integrated with a tapered Torsion Zone, the shank flexes under peak torque loads, preventing premature tip shear during high-power pneumatic or electric impact assembly.
Tungsten carbide consists of fine grains of tungsten carbide (WC) bound by a cobalt (Co) matrix. The grain size and cobalt percentage dictate performance:
PDC cutters are produced by sintering synthetic diamond particles with tungsten carbide substrates under ultra-high pressures (5.5 GPa) and temperatures (1400°C). The resulting cutter possesses unmatched micro-hardness (exceeding 8000 HV), enabling deep downhole drilling through abrasive quartz, granite, and hard rock formations.
As global manufacturing shifts toward Industry 4.0 automation, sustainability imperatives, and regional supply chain resilience, procurement directors must adapt to four transformative tooling trends:
Enterprise buyers are mitigating geopolitical freight risks by securing primary domestic suppliers (such as USA-based manufacturers) for critical custom reamers, step drills, and port contour tools.
Rather than scrapping worn tooling, re-sharpenable carbide tipped tools allow multiple regrind cycles, reducing virgin carbide consumption and lowering total lifecycle tooling costs by up to 40%.
Modern CNC tool bits feature laser-etched DataMatrix codes and RFID shanks to provide automated tool life management, feed rate optimization, and real-time wear prediction.
Furthermore, specialized manufacturing requirements—such as hydraulic manifold production according to MS16142, SAE J514F, SAE J1926, and MS33649 standards—require exporters with specialized port contour tooling capabilities. Single-pass porting tools cut seat, thread tap drill diameter, form angle, and spotface simultaneously, reducing multi-tool index times by over 65%.
For nearly four decades, Rock River Tool, Inc. has stood as a benchmark for American manufacturing excellence in carbide tipped and solid carbide cutting tools. Operating from dedicated facilities in the United States, Rock River Tool controls 100% of grinding, brazing, inspection, and finishing in-house. From standard jobbers length drills and chucking reamers to complex step tools, port contour cutters, and single point tools, our team delivers guaranteed geometric repeatability, application-matched carbide selection, and direct technical engineering support.
Comprehensive engineering guidance compiled by application specialists to address common procurement and operation challenges.
A carbide tipped tool brazes premium tungsten carbide tips exclusively at the cutting zone while maintaining a tough, shock-absorbing alloy steel body. This hybrid construction is ideal for interrupted cuts, cored castings, less rigid manual or older CNC machinery, and larger tool diameters (over 1/2 inch) where solid carbide becomes cost-prohibitive and susceptible to catastrophic fracture under flexure.
Standard chucking reamers are ground to nominal industry sizes with plus tolerances available upon request. For optimal hole size, roundness, and surface finish, leave approximately 0.010 in. to 0.015 in. of diameter stock for reaming operations. Always consult recommended speed and feed tables matching your specific workpiece hardness (e.g., cast iron vs. stainless steel).
Yes. Custom engineering is a core capability. We manufacture non-standard diameters, special flute lengths, step geometries, coolant-through modifications, custom shank flats, alternate carbide grades (C-2, C-5, C-6), and performance PVD coatings directly from customer prints or sample tool specifications.
For cast iron, aluminum alloys, brass, and abrasive non-ferrous materials, we recommend C-2 class carbide (such as our premium 883 grade) due to its exceptional resistance to abrasive wear. For carbon steels, alloy steels, and tool steels, C5/C6 class carbide (such as our 370 grade) is required to withstand higher thermal loads and prevent crater wear.
Physical Vapor Deposition (PVD) coatings apply a microscopic, high-hardness film (such as AlTiN or TiSiN) over the sharpened carbide cutting edge. This coating reduces coefficient of friction, prevents chip welding in sticky materials like aluminum or stainless steel, and acts as a thermal barrier permitting higher Surface Feet per Minute (SFM).
Connect with our application engineers for custom tool design, catalog quotes, volume exporter discounts, and direct technical support.