Rock River Tool, Inc.Precision Cutting Tools
Technical Support(800) 345-8924
Talk to an Engineer Direct from China's premier high-speed steel and micrograin solid carbide reamer manufacturing facilities. Customized geometry for lathe, CNC machining center, and manual high-accuracy hole finishing.
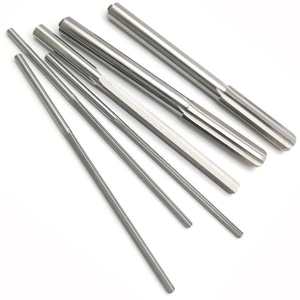
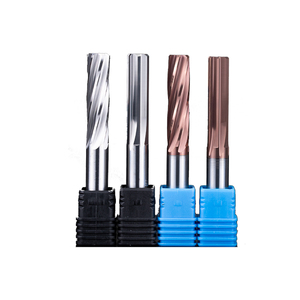
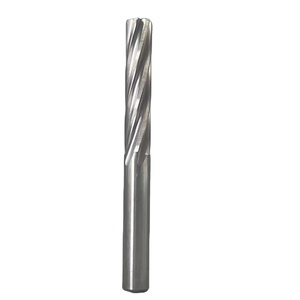
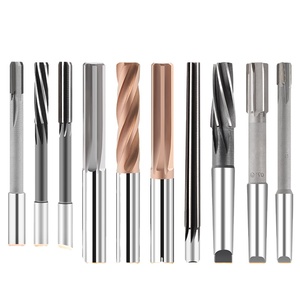
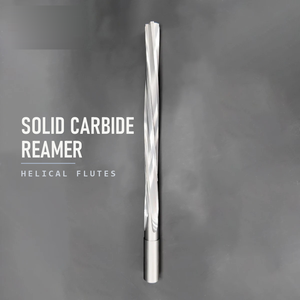
Modern precision manufacturing across automotive powertrain, aerospace hydraulics, medical device tooling, and defense production demands hole geometry accuracy measured in single-digit micrometers. While standard drilling operations create initial hole locations, finishing operations require specialized sizing tools. Procurement officers searching for the "China Best Spiral Reamer Factories & Factory" encounter thousands of vendors; however, identifying qualified tooling partners requires understanding the mechanical advantages of spiral flute geometry over traditional straight-flute tools.
Spiral reamers—engineered with helical flutes (typically ranging from 7° to 45° helix angles)—solve two critical mechanical challenges in hole finishing: chip accumulation in blind holes and chatter in interrupted cuts. Unlike straight-flute reamers that push chips forward or drag them along the wall, spiral flutes act as a continuous screw mechanism. Left-hand spiral/right-hand cut reamers push chips forward through through-holes, while right-hand spiral/right-hand cut tools pull chips upward out of deep blind holes, preventing scoring of the micro-finished surface.
Helical flutes draw metallic swarf away from the cutting zone, maintaining pristine surface finishes down to Ra 0.4 μm.
Continuous edge engagement across cross-holes and keyways eliminates edge chipping common to straight-flute cutters.
Leading Chinese factories grind tools on 5-axis CNC machines to achieve total indicated runout (TIR) under 0.002 mm.
The performance of a precision spiral reamer is determined before it ever touches a workpiece. Premier manufacturing facilities in Changzhou, Jiangsu, and Shenzhen invest in sub-micron grain tungsten carbide (WC-Co grade with 10-12% Cobalt binder) and M35/M42 Cobalt High-Speed Steels. The microscopic grain structure prevents intergranular failure under high mechanical shear strain.
A frequent error made by tooling buyers is specifying standard C-2 carbide for all non-ferrous work or standard C-5 for steel work without evaluating substrate thermal fatigue boundaries. Chinese tier-1 factories utilize application-matched grades:
| Tool Class | Core Material | Target Workpiece Hardness | Helical Flute Configuration | Achievable Tolerance |
|---|---|---|---|---|
| HSS-Co5 (M35) Machine Reamer | Cobalt Alloy HSS | < 32 HRC (Structural Steels, Al) | 15° Left-Hand Spiral / Right Cut | ISO H7 / H8 |
| Solid Carbide Micrograin Reamer | WC + 10% Co (0.4μm) | < 55 HRC (Tool Steels, Stainless) | 45° High Shear Spiral | ISO H6 / H7 |
| Brazed Carbide Tipped Reamer | C2/C5 Tip + 4140 Steel Body | < 45 HRC (Cast Iron, Forgings) | 12° Slow Spiral / Straight Shank | ISO H7 |
| Coolant-Fed Carbide Reamer | Solid Carbide (Internal Oil Hole) | < 65 HRC (Hardened Dies, Superalloys) | Internal Coolant + 30° Helix | ISO H5 / H6 |
As manufacturing transitions toward automated Industry 4.0 CNC cells, procurement requirements for reaming tools have shifted dramatically from basic stock replenishment to comprehensive Tool Life Optimization (TLO). Leading Chinese OEM/ODM factories are expanding their capabilities to support four major global procurement trends:
Modern machine centers operating at 70+ bar coolant pressure utilize spiral reamers with dual radial internal coolant holes. Fluid lubricates the margin directly at the shear zone, extending tool life by 300% in nickel superalloys.
Replacing traditional TiN coatings, factories now deposit nano-structured AlTiN, AlTiSiN, and Diamond-Like Carbon (DLC). These multi-layer physical vapor coatings withstand thermal gradients exceeding 1,100°C during dry reaming.
Single-pass reaming that produces multi-diameter bores, 7°/10° chamfers, and precise ball sockets reduces total cycle times for aerospace valve bodies and automotive steering knuckles.
When auditing top Chinese factories for OEM custom manufacturing or distributor partnerships, verified engineering systems separate high-tier producers from low-cost resellers. The manufacturing facility behind this technical portfolio adheres to rigid aerospace-grade quality protocols:
Utilizing 5-axis WALTER and ANCA CNC cutter grinders paired with high-frequency vacuum induction silver-brazing setups. This guarantees that brazed carbide tips maintain a joint shear strength exceeding 320 MPa.
Every batch undergoes automated 3D optical scanning to record cutting edge micro-geometry, lead chamfer angle accuracy, circular margin land width, and concentricity before surface coating.
Every carbide rod and alloy steel stock is cataloged with mill certificates. Traceable lot control ensures consistent hardness, density, and grain uniformity across batch reorders.
Need custom tool geometry, OEM distributor pricing, or technical speed/feed recommendations for your machining line? Contact our application engineering desk today for rapid engineering prints and factory-direct quotations.
Send an Inquiry