
MADE IN USA  Carbide Tipped & Solid Carbide Cutting Tools — manufacturing since 1986
Mon–Fri 7:00am–5:30pm CDT · (800) 345-8924
0%

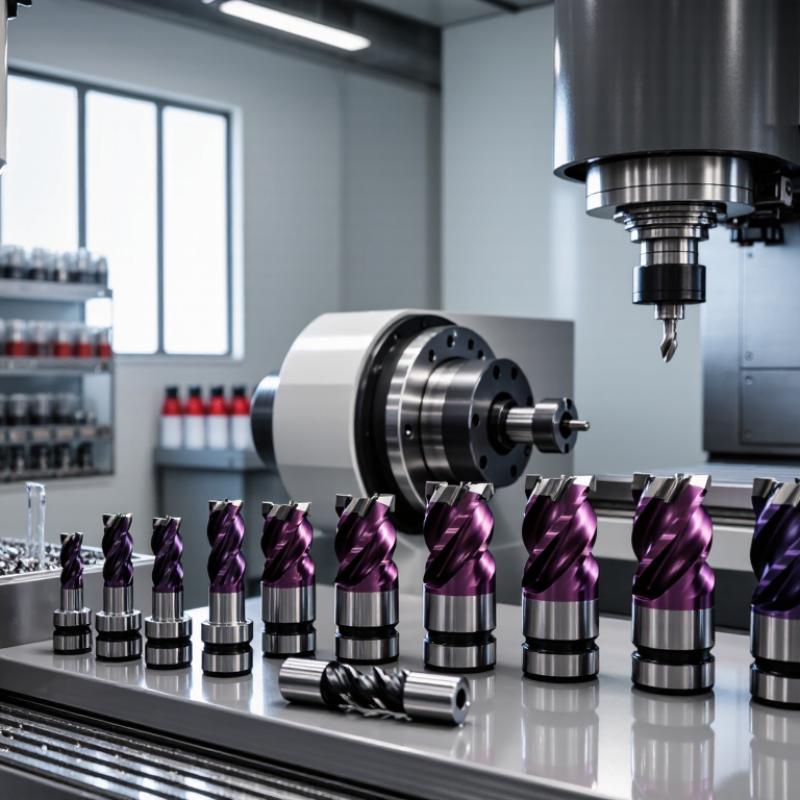
Choosing the right Stub Length CNC Drills in 2026 requires more than comparing prices or catalog photographs. Global buyers need tools that match machine capability, workpiece material, hole depth, and production volume. A short, rigid drill can reduce tool deflection during compact machining operations. It may also improve hole accuracy when spindle runout is controlled. Small details matter.

This guide examines leading Stub Length CNC Drills for international purchasing teams, machine shops, and industrial distributors. It considers carbide and high-speed steel options, point geometry, flute design, coatings, shank tolerance, and available diameter ranges. Application experience shows that aluminum, stainless steel, cast iron, and hardened alloys require different cutting strategies. A TiAlN coating may support higher heat resistance, while an uncoated drill can remain practical for softer materials and lower-speed work. Coolant access, chip evacuation, and machine rigidity also deserve careful review.

Supplier reliability is equally important. Buyers should verify inspection records, material certificates, dimensional consistency, packaging quality, and replacement support before placing large orders. Standards and import requirements can differ across regions. Check them carefully. No ranking is perfect. A drill that performs well in a German production cell may behave differently on an older machine in Brazil or Southeast Asia. This overview therefore balances published specifications with practical selection factors, test-cut evidence, and the limitations of available information. The goal is a dependable starting point, not an unquestionable verdict.
2026 Top Stub Length CNC Drills for Global Buyers

What Stub Length CNC Drills Are and Why Global Buyers Choose Them

2026 Top Stub Length CNC Drills for Global Buyers

What Stub Length CNC Drills Are and Why Global Buyers Choose Them

Stub length CNC drills have a shorter flute and overall body than standard-length drills. This compact geometry keeps the cutting edge closer to the tool holder. That detail matters during CNC work. Less reach usually means less deflection, reduced vibration, and cleaner hole locations. Machinists often choose them for steel plates, aluminum components, and compact fixtures. Still, short does not mean universal.

Global buyers value predictable performance across different machines and production sites. A stub drill can fit restricted work envelopes and leave more clearance around clamps. Its shorter body also supports stable drilling when the setup is rigid and properly aligned. In my production experience, accurate tool holding matters as much as drill geometry. Runout, spindle condition, and workholding can quickly erase the expected advantage. That is an easy detail to overlook. Buyers should check diameter tolerance, point angle, substrate, coating, and coolant compatibility. These details affect tool life and hole quality.

Reliable suppliers should provide inspection data, application guidance, and consistent batch control. International purchasing also requires clear dimensions, packaging protection, and documentation for customs and quality teams. Do not select a drill by price alone. A low-cost tool may produce burrs, oversized holes, or frequent changes. I have also seen premium specifications fail when operators used excessive feed or poor clamping. Selection needs testing. One trial hole can reveal more than a polished catalogue description. That practical check remains important when materials, machines, and operators vary between countries.

Key Design Features That Affect Stub Drill Performance

2026 Top Stub Length CNC Drills for Global Buyers

Stub drill performance depends on geometry more than appearance. A short flute reduces bending, especially when the tool enters steel plate or cast components. However, excessive stiffness can increase entry shock. The point angle must match the material, while a thicker web improves strength but raises cutting pressure. A balanced helix also helps move chips away from shallow holes.

Grand View Research valued the global CNC machine market at about USD 88 billion in 2023. Its report expects strong growth through 2030, increasing demand for repeatable drilling tools. That growth makes runout control important. Even 0.01 mm of runout can load one cutting edge harder than the other. Margin width, coating selection, and coolant access then affect heat and hole quality. These details are easy to overlook.

Tips: Check the drill’s actual diameter, point geometry, and maximum recommended depth. Test two feeds, not one. A perfect catalog value may fail on a rigid, interrupted setup. Record spindle load, burr size, and hole diameter after 20 holes. ISO 13399 tool data can support consistent purchasing, but it cannot replace a shop trial. Mistakes still happen. That is useful evidence.

2026 Top Stub Length CNC Drills for Global Buyers

Key design features that affect stub drill performance

The chart uses a normalized engineering index from 0 to 100 to compare how common stub-drill design features influence rigidity, chip evacuation, heat control, and hole accuracy. Short flute length and a thicker web generally improve stiffness, while point angle and helix angle must be matched to the workpiece material and cutting conditions.

How to Compare Materials, Coatings, Sizes, and Cutting Specifications

2026 Top Stub Length CNC Drills for Global Buyers

Comparing stub length CNC drills starts with the workpiece, not the catalog price. A short drill reduces deflection and improves control in compact machining areas. I once selected a low-cost tool for stainless steel and saw edge wear after only a few holes. That mistake showed me how strongly material choice affects tool life. Carbide suits hard alloys and high-volume production, while high-speed steel offers easier sharpening and lower entry cost. Coatings also matter. A wear-resistant coating can reduce friction, but its benefit depends on heat, speed, and coolant conditions. Check the coating temperature range and substrate compatibility.

Size selection requires more than matching the hole diameter. Match the drill diameter to the finished tolerance and allow for material springback. Do not assume every metric and inch size is interchangeable. Cutting specifications should include spindle speed, feed per revolution, point angle, and flute geometry. A 135-degree point can help reduce walking on many metal surfaces. Flute count affects chip evacuation, especially in deeper holes. Review the manufacturer’s tested parameters, then adjust them on your machine. Real cutting data matters. Shop rigidity, coolant delivery, and workholding can change results considerably. I still treat published figures as starting points, not promises. A trial hole, measured with a calibrated gauge, often reveals more than a polished specification sheet.

2026 Top Stub Length CNC Drills for Global Buyers - How to Compare Materials, Coatings, Sizes, and Cutting Specifications

Size / Drill Type Typical Diameter Range Standard Stub-Length Geometry Body Material Coating Options Shank / Tolerance Recommended Workpiece Materials Typical Cutting Speed Feed per Revolution Recommended Hole Depth Key Selection Notes
Micro stub drill 0.50–1.50 mm Approx. 2–3×D flute length; 30–38 mm overall length Solid carbide Uncoated, TiAlN, or AlCrN Cylindrical precision shank; commonly h6 Aluminium alloys, brass, cast iron, hardened steels 60–180 m/min, depending on material and coating 0.005–0.025 mm/rev Up to 2×D without pecking when chip evacuation is stable Requires high spindle accuracy, rigid fixturing, and filtered coolant.
Small-diameter stub drill 1.60–3.00 mm Approx. 2.5–3×D flute length; 34–46 mm overall length Solid carbide or cobalt-alloy HSS TiN for general use; TiAlN for heat-resistant alloys Cylindrical shank; h6 or h8 according to tool design Mild steel, stainless steel, aluminium, brass 25–100 m/min for HSS; 80–220 m/min for carbide 0.015–0.060 mm/rev 1.5–3×D; use peck cycles in gummy or stainless materials A split point or four-facet point reduces walking and thrust force.
General-purpose stub drill 3.20–6.00 mm DIN 1897-style short geometry; flute length typically 2.5–4×D High-speed steel, cobalt HSS, or solid carbide Uncoated, black oxide, TiN, TiAlN, or AlCrN Cylindrical shank; h8 is common for general-purpose tools Carbon steel, alloy steel, cast iron, aluminium alloys 20–45 m/min for HSS; 80–180 m/min for carbide 0.04–0.16 mm/rev 2–4×D, subject to flute length and chip control The best all-round option for rigid CNC milling and drilling centers.
Medium-diameter stub drill 6.10–10.00 mm Short series geometry; flute length typically 3–4×D Cobalt HSS or solid carbide TiN for general steel; TiAlN or AlCrN for higher heat loads Cylindrical shank; h8 or precision-ground shank Structural steel, stainless steel, cast iron, nickel-free heat-resistant alloys 18–35 m/min for HSS; 60–150 m/min for carbide 0.10–0.28 mm/rev 2–3×D for stable production drilling Use internal coolant where available for stainless steel and deep chip loads.
Large stub drill 10.10–16.00 mm Short, rigid body; flute length commonly 3–4×D Cobalt HSS or solid carbide with reinforced web TiAlN or AlCrN for alloy and stainless steels; TiN for lower heat loads Cylindrical shank; shank diameter must match the tool holder capacity Low-carbon steel, alloy steel, cast iron, aluminium 15–30 m/min for HSS; 50–120 m/min for carbide 0.18–0.40 mm/rev Up to 2.5×D; reduce feed when entering interrupted surfaces A rigid short drill reduces deflection but needs adequate torque and coolant flow.
Aluminium-optimized stub drill 2.00–12.00 mm Short flute length; 118°–140° point angle; polished flute surfaces Fine-grain solid carbide or HSS Uncoated polished surface or low-friction DLC-type coating Precision cylindrical shank; h6–h8 depending on holder Wrought aluminium, cast aluminium, copper alloys, magnesium alloys 100–300 m/min for carbide; 40–100 m/min for HSS 0.04–0.25 mm/rev 2–4×D with strong air blast or flood coolant High rake, polished flutes, and chip evacuation help prevent built-up edge.
Stainless-steel stub drill 2.00–16.00 mm Short rigid body; 135° split point is commonly used Cobalt HSS or solid carbide TiAlN, AlCrN, or multilayer heat-resistant coating Precision cylindrical shank; rigid hydraulic or shrink-fit holding preferred Austenitic and martensitic stainless steels 12–25 m/min for HSS; 35–90 m/min for carbide 0.05–0.22 mm/rev 1.5–2.5×D; peck only when needed to avoid work hardening Maintain positive feed and avoid dwelling at the hole bottom.
Cast-iron stub drill 3.00–16.00 mm Short body; 118°–135° point angle depending on grade Cobalt HSS or solid carbide TiN, TiAlN, or AlCrN; uncoated carbide may suit dry drilling Cylindrical shank; rigid clamping required Grey cast iron, ductile iron, compacted graphite iron 15–35 m/min for HSS; 50–140 m/min for carbide 0.08–0.30 mm/rev 2–3×D; use air blast to clear abrasive chips Dry cutting is often practical, but dust extraction and edge protection are important.
Hardened-steel stub drill 2.00–12.00 mm Short reinforced geometry; point angle commonly 135°–140° Fine-grain solid carbide AlCrN, AlTiN, or other high-temperature PVD coating High-precision shank; runout should typically be held below 0.01 mm Pre-hardened and hardened steels, approximately 45–60 HRC 20–60 m/min, depending on hardness, tool grade, and coolant 0.02–0.12 mm/rev 1–2×D; use stable interpolation or peck cycles for difficult holes Prioritize edge strength, low runout, and a rigid machine-tool setup.
Inch-size stub drill #80–1/2 in Short-series dimensions vary by inch drill standard; flute length typically 2.5–4×D HSS, cobalt HSS, or solid carbide Uncoated, black oxide, TiN, TiAlN, or AlCrN Inch cylindrical shank; verify shank size and holder compatibility General engineering steels, aluminium alloys, cast iron, stainless steel Use the equivalent metric material range after converting diameter Use the equivalent metric feed after converting diameter Normally 2–4×D; confirm the exact tool drawing before production use Confirm fractional, letter, and number gauge dimensions before ordering.
Comparison and calculation notes:
  • Cutting speed values are typical starting ranges, not universal limits. Adjust them for machine rigidity, coolant, tool overhang, workpiece hardness, and hole quality requirements.
  • Spindle speed can be calculated as n = (1000 × Vc) ÷ (π × D), where n is rpm, Vc is cutting speed in m/min, and D is drill diameter in mm.
  • For CNC production, a short, rigid drill is generally preferred when the required hole depth remains within the effective flute length and chip evacuation is reliable.
  • Always verify the exact dimensional standard, point geometry, tolerance, coating thickness, and manufacturer cutting chart before commercial production.

Top Stub Length CNC Drill Types for Different Machining Applications

Top Stub Length CNC Drills for Global Buyers

Stub length CNC drills suit applications that demand rigidity, accurate positioning, and limited tool projection. Their shorter body reduces deflection during drilling. This benefit is noticeable when machining steel plates, aluminum housings, and compact components.

Short tools matter. A standard two-flute general-purpose drill works well for stable machines and common materials. Its split point can reduce wandering on prepared surfaces. However, it may struggle when chip evacuation becomes difficult.

Carbide stub drills are suitable for high-volume production, hardened alloys, and machines with strong spindle stability. They maintain cutting performance at higher speeds, but they are less forgiving of vibration or poor alignment.

Cobalt alloy drills offer a practical option for stainless steel and heat-resistant materials. Their toughness helps with interrupted cuts, though excessive feed can still create heat and edge damage. Coolant delivery should reach the hole entrance, not merely flood the work area.

For deep or blind holes, a short drill may need peck cycles and careful chip control. Through-coolant support can improve consistency, especially in automated production.

Buyers should compare point angle, coating suitability, tolerance, shank size, and available machining data. Machine runout also deserves attention; a precise drill cannot correct a misaligned holder.

No selection chart is perfect. Material batches vary, and real cutting tests remain necessary.

I have seen a seemingly ideal drill fail because the workholding was too flexible. Test before scaling.

Global Buying Factors: Quality, Compatibility, Pricing, and Supply Support

2026 Top Stub Length CNC Drills for Global Buyers

Global buyers should assess stub length CNC drills beyond the catalog price. In practical sourcing work, tight runout and consistent point geometry often determine hole quality. Ask for inspection data, material specifications, and sample results before placing a large order. A drill that leaves a clean hole at 3,000 rpm can reduce rework and tool changes. However, quality claims still need verification.

Compatibility deserves equal attention. Confirm shank diameter, flute length, point angle, and workpiece material with the supplier. Check whether the drill suits your holder, coolant method, and machine clearance. Pricing should include shipping, taxes, packaging, expected tool life, and replacement rates. The lowest quote may become expensive after frequent breakage. A perfect buying formula does not exist.

Tips: Request a small trial batch. Measure hole diameter and surface finish. Compare tool life under your actual cutting conditions. Keep written tolerances and delivery dates. Ask how damaged tools are handled. Supply support matters during production delays, especially when replacement stock is limited. Reliable suppliers should provide clear lead times, stable packaging, and responsive technical communication. Yet buyers should not assume every promise is equally dependable; documented performance is stronger than confident wording.

FAQS

Why are stub length CNC drills useful in compact machining areas?

Their shorter bodies reduce tool projection and deflection. This improves positioning control. Short tools matter. They work well for steel plates, aluminum housings, and compact components. However, flexible workholding can still cause poor holes.

Which drill material suits different workpiece materials?

Carbide suits hard alloys and high-volume production. High-speed steel costs less and allows easier sharpening. Cobalt alloy drills suit stainless steel and heat-resistant materials. Material choice strongly affects tool life. I once chose cheaply and learned this late.

How should buyers compare drill coatings?

Check the coating temperature range and substrate compatibility. A wear-resistant coating may reduce friction and edge wear. Its benefit depends on speed, heat, and coolant delivery. Do not trust the coating name alone. Actual cutting results matter more.

How do I choose the correct drill size?

Match the drill diameter with the finished hole tolerance. Allow for material springback. Metric and inch sizes are not automatically interchangeable. Check shank diameter, flute length, and holder compatibility. Measure a trial hole with a calibrated gauge.

Which cutting specifications should be reviewed?

Review spindle speed, feed per revolution, point angle, and flute geometry. A 135-degree point can reduce walking on many metal surfaces. Flute count affects chip evacuation. Published figures are starting points, not promises.

Are stub drills suitable for deep or blind holes?

They can work, but chip control becomes more difficult. Peck cycles may be necessary. Through-coolant can improve consistency in automated production. Coolant should reach the hole entrance. Short drills are not automatically ideal for deep holes.

How does machine condition affect drilling performance?

Machine rigidity, runout, coolant delivery, and workholding can change results considerably. A precise drill cannot correct a misaligned holder. Vibration can damage carbide edges quickly. The chart may be right, but your machine may disagree.

What should global buyers check before placing a large order?

Request inspection data, material specifications, and sample results. Confirm shank size, point angle, flute length, and workpiece compatibility. Include shipping, taxes, packaging, tool life, and replacement rates. Ask about damaged tools and delivery dates. No shortcut exists.

Why is a trial batch important?

A small trial batch reveals real tool performance before wider purchasing. Measure hole diameter and surface finish. Compare tool life under actual cutting conditions. Keep written tolerances and delivery dates. Test before scaling.

Conclusion

Stub Length CNC Drills are compact, rigid cutting tools designed for accurate holemaking in CNC machining environments. Their shorter working length helps reduce tool deflection, improve stability, and support consistent results during drilling operations. This article explains how flute geometry, point design, core strength, shank accuracy, and coolant channels influence drill performance. It also outlines how buyers can compare carbide and high-speed steel options, surface coatings, diameters, point angles, cutting speeds, feed rates, and depth capabilities according to material and production requirements.

Different Stub Length CNC Drills are suited to general-purpose machining, hardened materials, aluminum, stainless steel, cast iron, and high-volume manufacturing. For global buyers, selecting the right product involves more than comparing unit prices. Quality consistency, machine and holder compatibility, dimensional standards, coating reliability, packaging, lead times, minimum order quantities, technical documentation, and after-sales support are equally important. A balanced evaluation helps buyers achieve dependable performance, lower tool consumption, and stable long-term supply.
Isla

Isla

Isla is a dedicated marketing professional with a strong understanding of product strategy, customer needs, and market trends. As a key contributor to the company’s communications team, Isla regularly updates the company website with clear, practical, and insightful blog articles that help readers......